作者: l, xt

  • How Should Buyers Interpret Fabric Opacity Test Results for Activewear Fabric?

    How Should Buyers Interpret Fabric Opacity Test Results for Activewear Fabric?


    Buyers should interpret an opacity result only when the test method, fabric color, backing, conditioning, measurement geometry, and stretch state are stated. A high relaxed opacity value does not prove that leggings, sports bras, or shapewear will remain covered when the fabric is stretched, wet, or assembled into a garment.
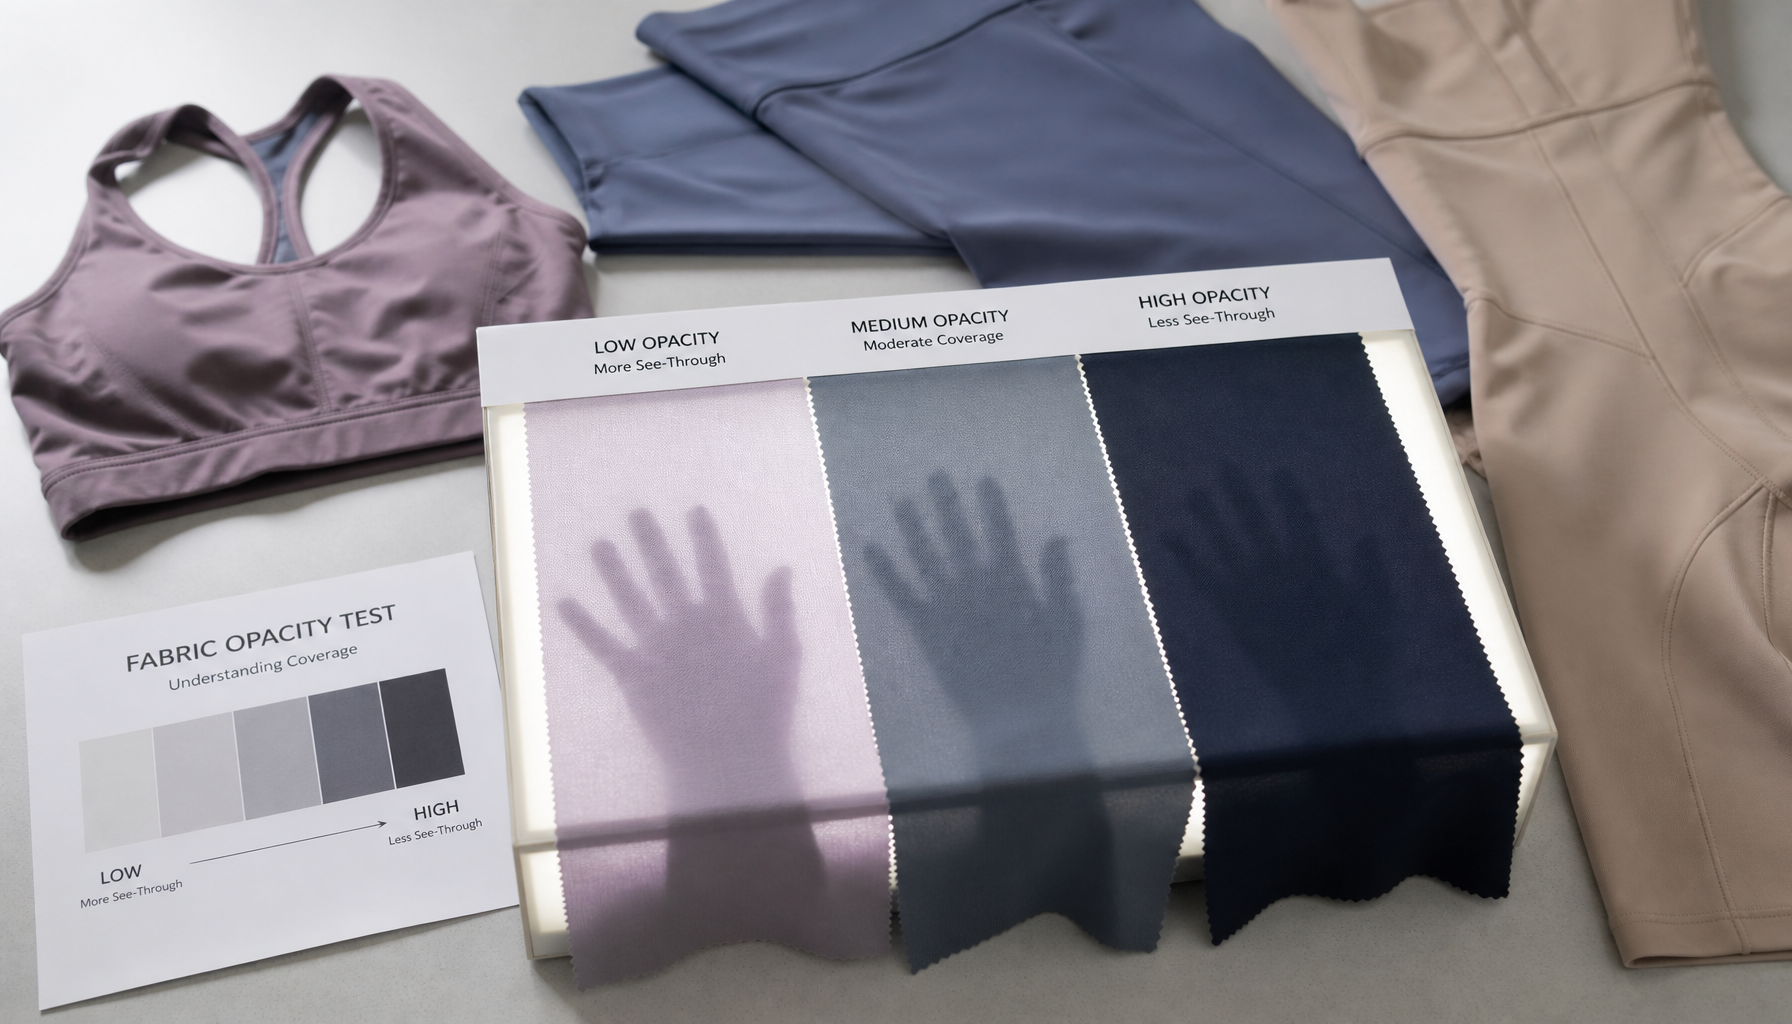
    Activewear fabric sample prepared for opacity evaluation

    Confirm what the reported number represents

    “Opacity,” “light transmission,” and “coverage” are related but not interchangeable terms. An opacity value generally increases as less light is visible through the specimen, while a transmission value moves in the opposite direction. The report must define the measured property and calculation; buyers should not assume that opacity is simply 100% − transmission unless the stated method uses that relationship.

    Before comparing two reports, confirm:

    • the test method and instrument;
    • illumination and detector geometry;
    • backing color or reference standard;
    • specimen color and dye lot;
    • aperture size and number of readings;
    • conditioning and wet or dry state;
    • whether the fabric was relaxed or extended;
    • extension direction and percentage.

    Results produced under different conditions may describe different optical behavior even when both documents use the word “opacity.”

    Evaluate opacity at the garment's working extension

    Activewear fabrics open between loops and become thinner when stretched. This can expose the wearer or a contrasting underlayer even when the relaxed swatch appears opaque. The buyer should therefore define the extension expected at the seat, thigh, knee, bra cup, or shapewear panel and request measurements or visual assessments at that condition.

    Illustrative calculation — not a ClothFactory test result: assume a 100 mm fabric section is extended to 150 mm in one direction while the other dimension remains unchanged. Its area increases by 50%:

    150 mm ÷ 100 mm = 1.50

    The same fabric mass is then distributed across approximately 1.5 times the original area, so the mass per projected area becomes about:

    1 ÷ 1.50 = 0.667, or 66.7% of the relaxed value.

    This simplified geometry explains why coverage can fall under extension, but it does not predict the final opacity value. Loop deformation, yarn shape, fabric thickness, color, and finishing change the optical response and must be measured on the actual sample.
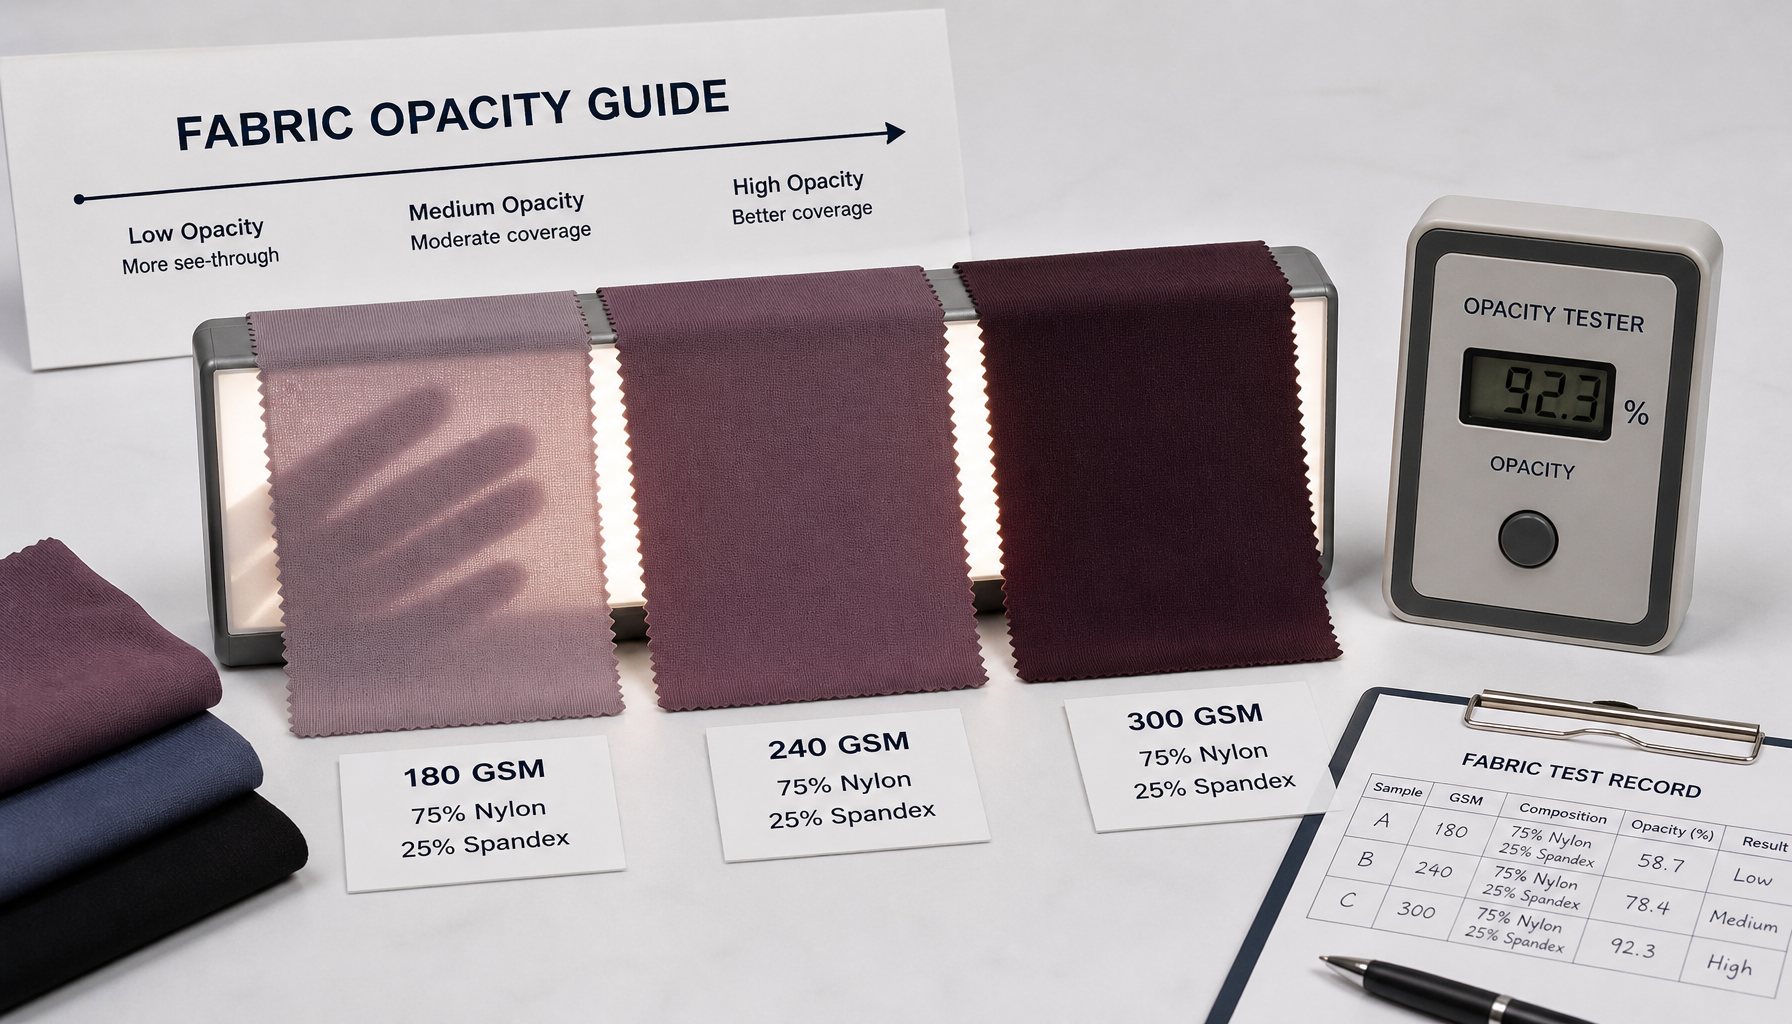
    Stretch activewear fabric being checked for coverage and show-through

    Compare color, construction, and finish separately

    The same knit construction can produce different opacity results across colors. Dark shades often mask contrast differently from pale or bright shades, but no color should be accepted by assumption. Test the commercially important shades or define a risk-based color plan that includes the shades most likely to show contrast.

    GSM, thickness, yarn size, knit density, and surface finish all influence coverage, but none is a standalone guarantee. A higher-GSM fabric can still become visibly open under stretch, while a lower-GSM construction may maintain coverage through tighter loop geometry or different yarn selection. Compare the finished fabric, not just nominal composition or greige specifications.

    If moisture-management, brushing, heat setting, or another finish is applied, repeat the relevant opacity assessment after the production finish and agreed wash cycle. An optional finish should not be described as a default property of every color or order.

    Match the test to the activewear application

    Application Critical viewing condition Additional approval check
    Yoga leggings Seat and thigh at the intended garment extension Squat and bend assessment on the correct size, color, and underlayer
    Compression shorts Sustained extension across seat and upper leg Recovery, seam distortion, and coverage after laundering
    Sports bras Cup and side panel over the intended lining or skin-tone contrast Coverage at extension, moisture exposure, and seam placement
    Shapewear High-extension control zones Local thinning, panel transitions, comfort, and residual growth
    Lightweight training tops Back and shoulder during movement Wet-state appearance, air permeability, and body-side contrast

    Laboratory readings help control material consistency. A garment trial confirms whether pattern dimensions, seam placement, panel orientation, lining, and wearer movement create an acceptable result. Neither step should replace the other.

    Define acceptance against a reference, not a universal number

    There is no single opacity percentage that is correct for every activewear product. Buyers should establish an approved reference fabric or garment and record the conditions under which it passes. The bulk requirement can then specify the same method, shade group, extension, backing, conditioning, and tolerance.

    A practical approval record should include:

    1. fabric code, composition, knit construction, finished GSM, and usable width;
    2. color and dye-lot identity;
    3. relaxed and extended test conditions;
    4. numerical results with individual readings, not only an average;
    5. an approved visual reference where appearance matters;
    6. wash or wet-state checks required by the product brief;
    7. the action required when a lot falls outside tolerance.

    Individual readings matter because an average can hide local variation caused by barre, uneven density, finishing variation, or specimen selection.

    Avoid common interpretation errors

    • Comparing percentages from different methods. Matching units do not make the results equivalent.
    • Approving only the relaxed fabric. Coverage can change materially at the garment's working extension.
    • Using GSM as an opacity guarantee. Weight does not describe loop opening, thickness, or color contrast.
    • Testing one shade for the complete range. Color and dyeing conditions can change perceived and measured coverage.
    • Ignoring the backing. A white, black, or skin-tone backing can produce a different visual conclusion.
    • Relying only on a squat photo. Camera exposure, lighting, underwear color, pose, and image processing make uncontrolled photos difficult to compare.
    • Treating fabric data as a garment result. Pattern strain, seams, panels, and sizing affect final show-through.

    Information to request from the supplier

    Ask for the full opacity report, not a single percentage copied into a product sheet. The report should identify the sample, method, instrument conditions, color, backing, specimen state, extension, number of readings, and result range. Send the supplier the garment application, target fit, expected extension, shade plan, lining or underlayer, care cycle, and approved reference.

    ClothFactory can use those conditions to compare nylon-spandex or polyester-spandex candidates and prepare matched samples. Bulk approval should remain tied to the agreed test setup and garment verification rather than to an isolated opacity claim.
  • How Should Buyers Compare Suppliers of Fabric for Yoga Leggings?

    How Should Buyers Compare Suppliers of Fabric for Yoga Leggings?


    There is no universal sample count for checking fabric stretch ratio. The selected test method determines the required laboratory specimens, while the buyer's sampling plan must separately cover the rolls, dye lots, fabric directions, and locations needed to represent the sourcing decision.

    Define what “stretch ratio” means before sampling

    Suppliers and buyers may use “stretch ratio,” “elongation,” and “stretch percentage” differently. The test request should define the calculation and reporting unit instead of relying on the phrase alone.

    For percentage stretch:

    Stretch (%) = (extended length − initial length) ÷ initial length × 100

    Illustrative calculation — not a ClothFactory test result: a marked length that increases from 100 mm to 150 mm has:

    (150 mm − 100 mm) ÷ 100 mm × 100 = 50% stretch

    The same result could be described as an extended-length ratio of 1.5:1, so the report must state which convention it uses. It should also distinguish maximum extension from force at a specified extension, recovery after release, and residual growth. These values answer different procurement questions.

    Separate laboratory specimens from production coverage

    Stretch testing involves several sampling levels:

    • Production lot: the quantity covered by one acceptance decision.
    • Rolls or production groups: represent dye lots, knitting positions, finishing groups, dates, or other traceable sources.
    • Locations within a roll: reveal variation along the roll length or across its usable width.
    • Fabric directions: normally require separate evaluation because coursewise and lengthwise behavior can differ.
    • Test specimens: pieces prepared and measured according to the selected method.

    Several specimens cut beside each other improve repeatability for that sampled location, but they do not demonstrate consistency across multiple rolls. Ten specimens from one roll still represent one roll.

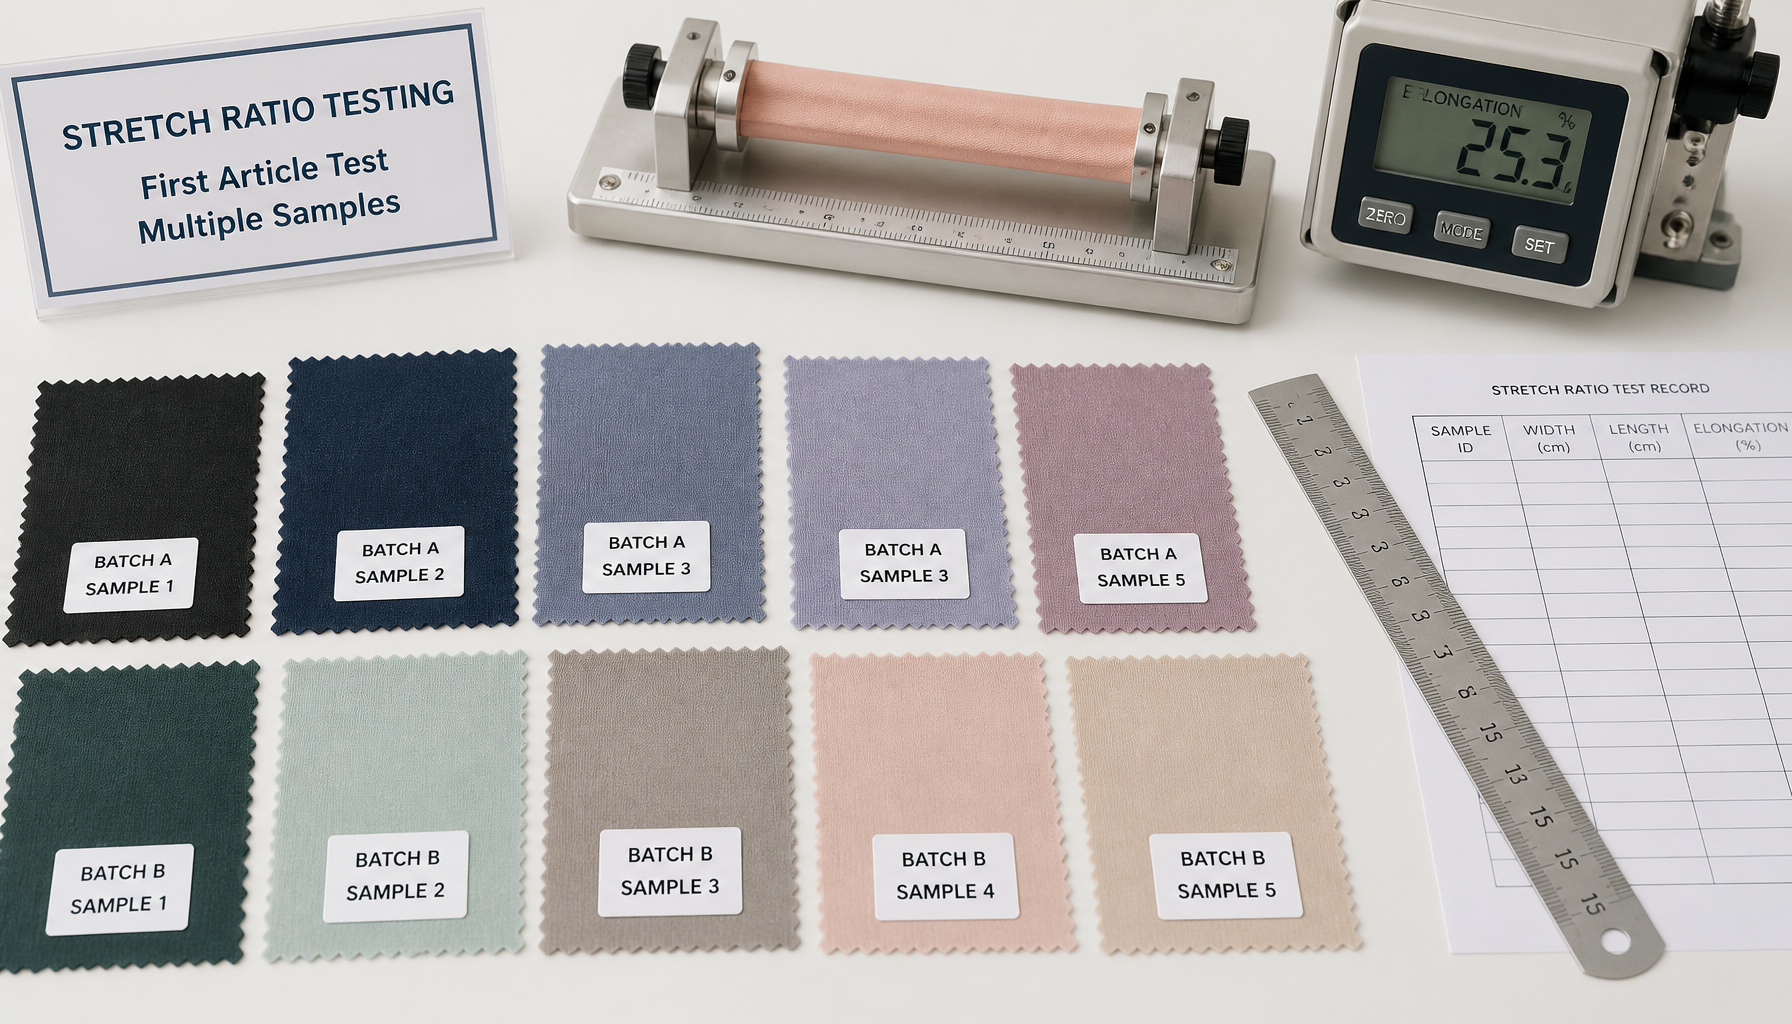
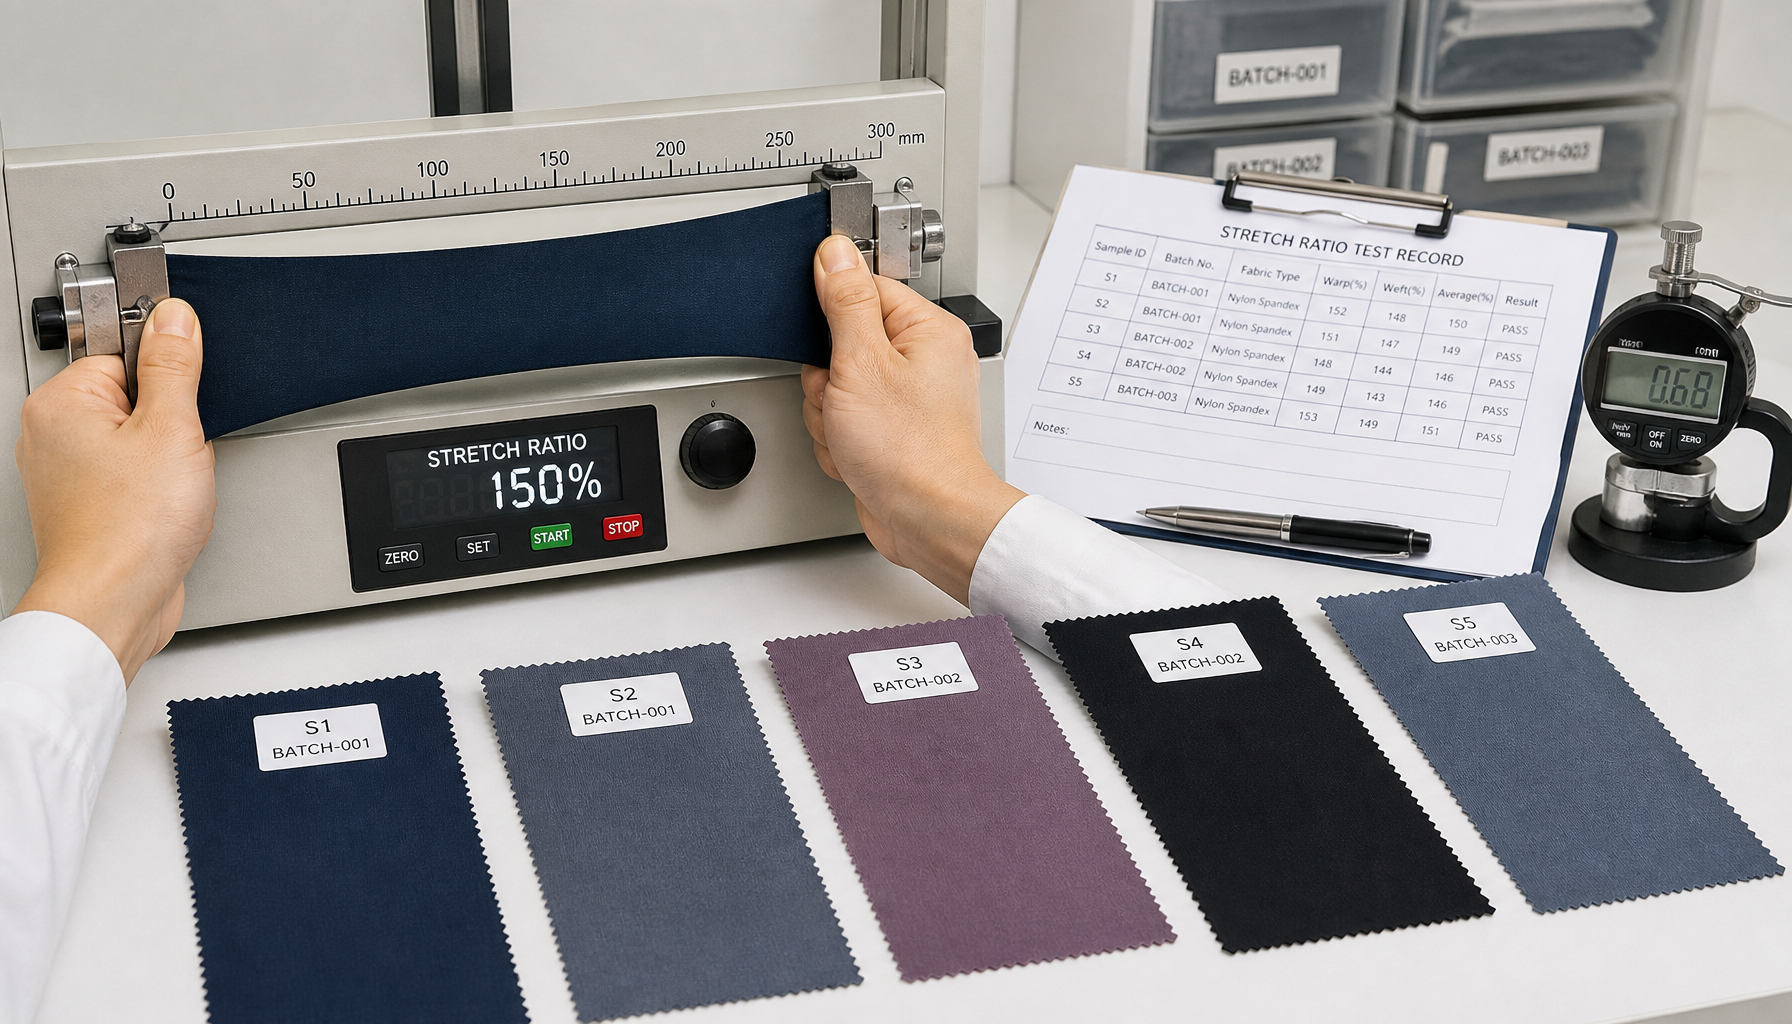
    Stretch fabric specimens prepared for elongation testing

    Let the test method set the specimen count

    Stretch methods differ in specimen dimensions, gauge length, load or force, extension rate, cycling, hold time, recovery time, and calculation. Select the method first, then complete its required specimen set for every sampling group in the buyer's plan.

    The report should state:

    • method identifier and edition;
    • specimen count and direction;
    • conditioning and relaxation procedure;
    • gauge length and specimen dimensions;
    • applied load or target extension;
    • extension rate, hold time, and number of cycles;
    • recovery interval and residual-growth calculation;
    • pre-wash or post-wash condition;
    • individual results, average, range, and specimen origin.

    Do not divide one method-required specimen set among unrelated rolls unless the method and purchase agreement explicitly permit that design.

    Knitted stretch fabric being measured under controlled extension

    Adjust production coverage to the sourcing stage

    Stage Decision being made Appropriate sampling logic
    Candidate screening Is this construction worth developing? Test one complete method-required set from each candidate under identical conditions. Results represent only the submitted samples.
    Finished-fabric development Did dyeing, heat setting, or another finish change the response? Test complete sets from matched, identified material before and after the relevant process or wash condition.
    Pre-production confirmation Is the approved construction reproducible? Cover more than one identified production position or roll where available, with complete sets for each sampling group.
    Bulk-lot acceptance Can the shipment be released? Select rolls across each defined dye lot or production group using a written contractual or risk-based plan.

    The plan should state how to handle an outlying roll or group. Options may include adjacent resampling, expanded roll coverage, investigation, segregation, reprocessing, or rejection. A passing overall average should not automatically release a roll with unacceptable recovery or force behavior.

    Use an illustrative sampling calculation correctly

    The following is a hypothetical buyer-defined plan, not an industry standard or ClothFactory test result. Suppose a buyer selects four representative rolls and samples two locations per roll:

    4 rolls × 2 locations = 8 sampling groups

    If both principal directions are evaluated separately:

    8 sampling groups × 2 directions = 16 direction-specific groups

    Each group must then supply the complete number of specimens required by the selected method. If that number is n, the total is:

    16 direction-specific groups × n method-required specimens

    The correct number of rolls depends on lot size, dye-lot structure, color and finish groups, earlier quality history, construction risk, and the purchase agreement. The example shows the calculation logic, not a default requirement.

    Measure more than maximum stretch

    Maximum elongation alone does not show whether a fabric will provide support or maintain fit. For leggings, sports bras, underwear, or shapewear, buyers may also need:

    • force at the extension expected in the garment;
    • recovery after a defined hold and relaxation period;
    • residual growth after repeated cycling;
    • results after the intended wash and drying procedure;
    • appearance, cover, or print integrity under an agreed extension.

    Spandex percentage is not a substitute for these measurements. Yarn size, knit geometry, spandex feeding, heat setting, finishing, and specimen direction all influence the result.

    Keep every comparison condition consistent

    Stretch results are comparable only when the conditions match. Use the same specimen direction, dimensions, conditioning, gauge length, load or extension, rate, cycles, hold time, recovery interval, and laundering condition across candidates.

    Record the exact fabric code, color, finish, roll, dye lot, and sampling location. Test the finished construction rather than relying only on greige fabric or an unfinished development swatch. Dark colors, special finishes, or different heat-setting conditions may need separate confirmation when they create a different production risk.

    Interpret variation before averaging

    Review individual and group results, not only the mean. A wide range can indicate variation by roll, direction, location, finish, or test preparation. Investigate that source before adding more results to an average.

    Retesting adjacent material can help determine whether an unusual result is local or representative, but the original result should remain in the record. The purchase agreement should define whether acceptance applies to each roll, each production group, or the lot as a whole.

    Information buyers should include in the request

    Provide the supplier or laboratory with:

    • fabric code, composition, knit construction, finished GSM, and usable width;
    • intended garment, body zone, fit, and expected extension;
    • selected test method and reporting convention;
    • specimen directions and production sampling locations;
    • conditioning, cycling, hold, recovery, and wash requirements;
    • required force, stretch, recovery, or growth limits;
    • lot definition and roll-selection rule;
    • report format showing individual results and full traceability.

    Procurement next step

    Choose the stretch method and reporting convention first. Then build a separate production sampling plan that covers the rolls, dye lots, directions, and locations relevant to the order. ClothFactory can prepare identified nylon-spandex or polyester-spandex specimens, but the buyer and supplier should agree the method, sampling coverage, garment extension, recovery interval, and acceptance limits before using the results for bulk approval.

  • How Should Apparel Brands Compare Sample-Yardage Plans Across Fabric Suppliers?

    How Should Apparel Brands Compare Sample-Yardage Plans Across Fabric Suppliers?

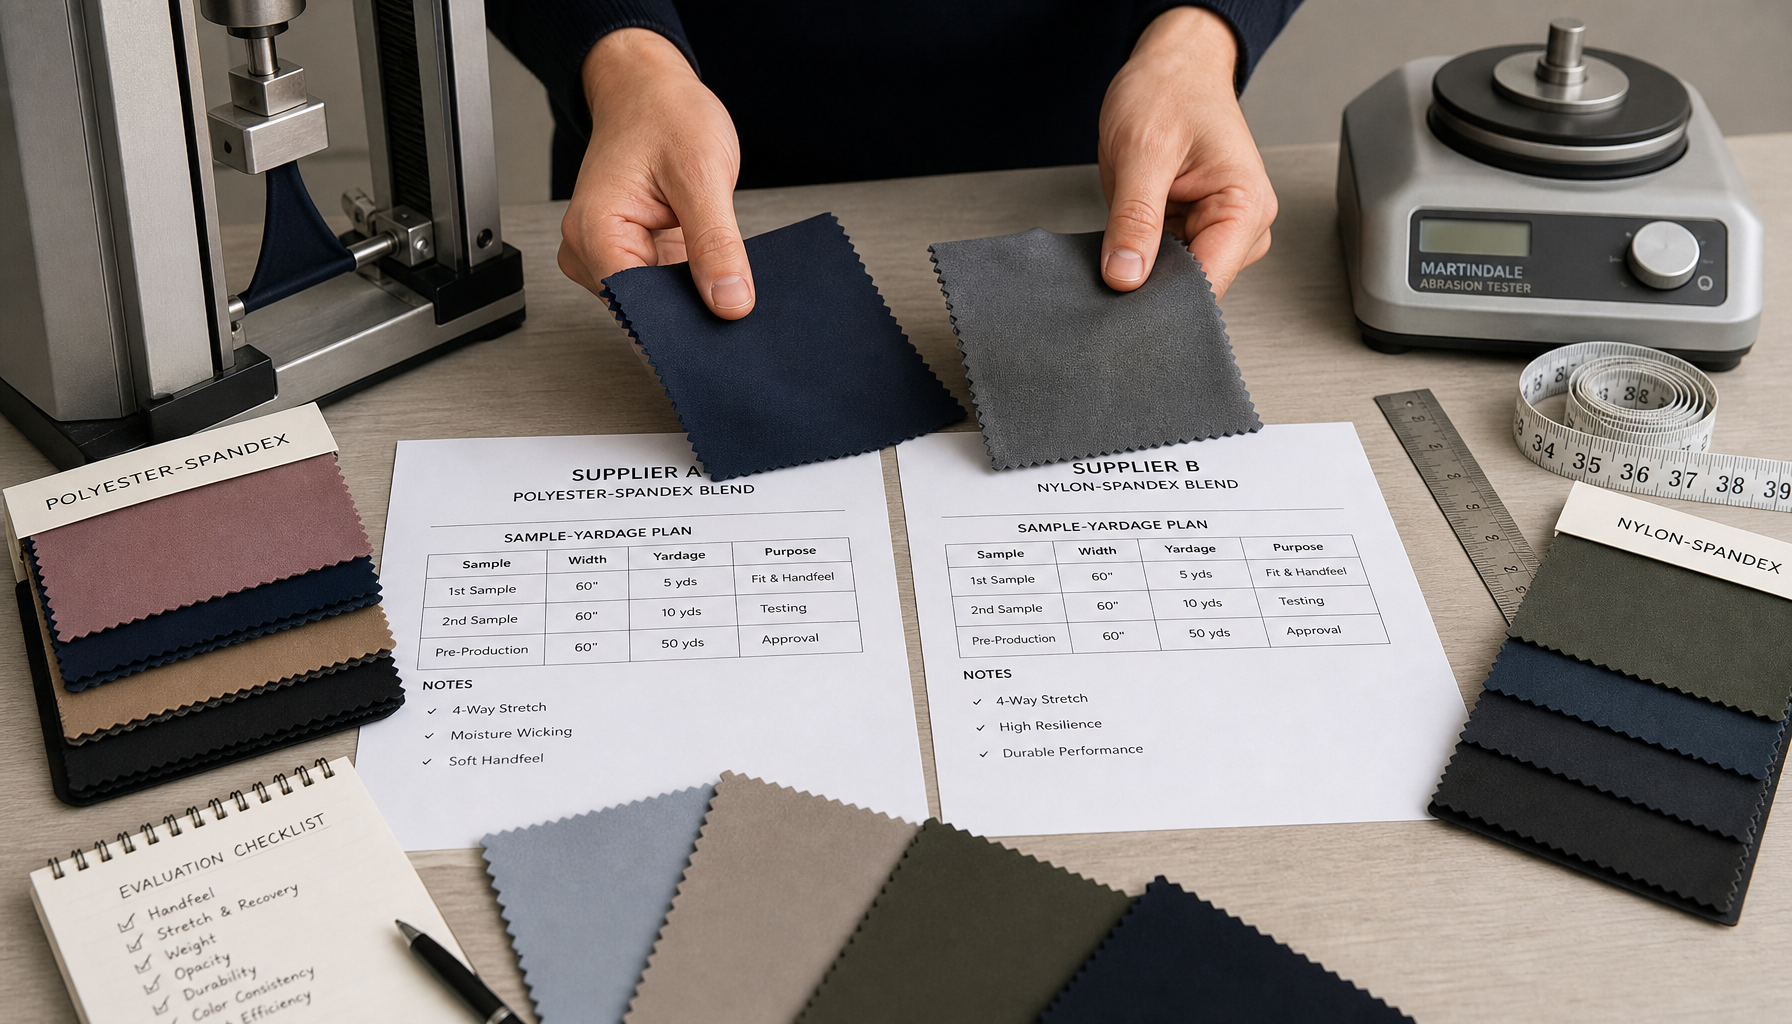
    Compare sample-yardage plans by the decisions they allow you to make, not by the number of free metres offered. A stock cutting, a development length and a production-representative sample may look similar but support different approvals. The useful plan provides enough correctly identified material for the required tests and garments without presenting unresolved assumptions as bulk approval.

    What is each sample intended to approve?

    Ask the supplier to state whether the material is for initial hand-feel selection, pattern development, colour approval, performance evaluation or production confirmation. A stock fabric can help establish a silhouette while differing from the proposed bulk colour or finish. That does not make it useless; it limits what the buyer can approve from it.

    Record known differences in yarn, construction, dyeing and finishing. A sample described only as “similar quality” cannot support a precise technical sign-off. Ask which differences will disappear in the next sample and which remain part of the commercial proposal.

    How much sample yardage is actually needed?

    Build the request from the sampling plan. Include the number of garments and sizes, laboratory specimen requirements, retained references and any second-round sewing trials. Confirm laboratory cutting instructions before allocating fabric; different methods and repeat counts need different quantities.

    In a hypothetical plan, six garments at 0.90 m each require 5.40 m. Adding an agreed 2.00 m for laboratory work and 1.00 m for retention gives 8.40 m before a separate contingency. The 2.00 m allowance is illustrative, not a universal laboratory requirement. Use consumption from a marker at the sample’s actual usable width.

    Confirm units. Ten yards equals 9.144 m, not 10 m. That 0.856 m difference could remove almost one garment from the illustrative plan. Specify whether the requested quantity must be one continuous full-width length or can include separate pieces.

    Is the sample representative of the proposed bulk order?

    Request the article revision, sample lot, colour, finish, measured weight and usable width. Ask whether the material was produced through the proposed bulk route or prepared using a different development process. A supplier should identify any remaining scale-up or process differences so the buyer can plan confirmation testing.

    For stretch activewear, a change in finish can alter hand feel and measured dimensions even when the commercial article name remains unchanged. Keep the approved cutting and a record of its preparation and care history. Do not approve production against memory of a sample viewed weeks earlier.

    How should we compare two different offers?

    Suppose Supplier A offers 12 m of stock fabric in a substitute finish, while Supplier B offers 9 m using the proposed production construction and finish. These are hypothetical offers. Against the 8.40 m plan, B appears sufficient before contingency only if width, continuity and specimen needs match the plan. A supplies more length but may leave performance and finish approval unresolved.

    Choose according to the development stage. A may be useful for an early pattern trial if the differences are acceptable and documented. B may reduce the need for a later material-confirmation round, but it still does not prove consistency of an unseen bulk lot. Compare the total number of remaining decisions, not just metres supplied.

    Which costs and timing terms should be written down?

    Separate fabric charges, development fees, colour charges, cutting fees, shipping and laboratory work. Confirm whether any fee is credited against an order, the conditions for that credit and whether a changed specification triggers another charge. “Free samples” can still create courier costs and repeat-development expense.

    Ask when the lead-time clock starts: brief acceptance, payment, yarn availability or colour approval. Distinguish material-ready dates from dispatch and receipt. Specify who approves substitutions; an unannounced substitute can arrive on time while failing to support the planned testing.

    How do we keep sample approvals traceable?

    Assign a sample identifier and keep it on the cutting, technical sheet, test request, garment and approval record. Record receipt date, usable dimensions, visible defects and deviations from the request before cutting. Reserve the retention piece so it is not consumed by an unexpected extra fitting.

    Use a change log to state what is approved, what is rejected and what remains open. If a fit sample passes but recovery testing fails, do not write a general “sample approved” message. State that pattern approval is conditional and material approval remains on hold pending the named correction and retest.

    What makes a sample plan ready to place?

    A workable plan identifies purpose, quantity, units, usable width, continuity, material revision, permitted differences, cost, timing and the next approval gate. It also assigns responsibility for test results and for replacing non-representative material.

    For a ClothFactory enquiry, send the garment brief and that sampling plan together. The aim is to purchase enough reliable information to decide whether to proceed, revise or stop. Extra yardage has little value if its identity and approval scope are unclear.

  • Which Knit Structure Should Buyers Consider for Golf Shirts?

    Which Knit Structure Should Buyers Consider for Golf Shirts?

    Pique, interlock and jersey are all candidates for golf shirts; none is automatically best. Choose the structure against the intended silhouette, playing conditions, logo process and care expectations. Fibre composition, yarn specification, fabric density and finishing must be considered alongside the knit name. A “performance pique” label is not evidence of airflow, recovery or moisture management.

    Start with the shirt’s commercial role

    A club-uniform polo may need a consistent textured appearance, reliable embroidery and repeat ordering. A lightweight tournament shirt may prioritise freedom of movement and reduced material mass. A premium travel polo may prioritise a smooth face and a stable silhouette. Those briefs can lead to different structures even when all three use polyester-spandex or nylon-spandex yarns.

    Set the non-negotiable requirements first: fit, opacity in selected colours, care procedure, logo method and target material cost. Treat hand feel and surface character as approved references rather than trying to describe every preference with “soft” or “premium.”

    Understand what each structure offers to the design

    Structure-based starting points, not guaranteed performance rankings
    Candidate Reason to sample it Question to resolve
    Pique A textured face associated with classic polo styling. Does the actual construction deliver the desired texture, snag resistance and logo appearance?
    Interlock A double-knit option for a smooth, substantial appearance. Can the chosen weight and finish meet the brief without excessive warmth or stiffness?
    Single jersey A candidate for a lighter, more fluid silhouette. Will edge behaviour, dimensional change and placket assembly remain controlled?

    Ask suppliers to identify the actual construction rather than relying only on a trade name. Pique variants can differ, and a photograph cannot reliably identify yarns or loop geometry. Compare finished samples with their technical sheets and relevant measurements.

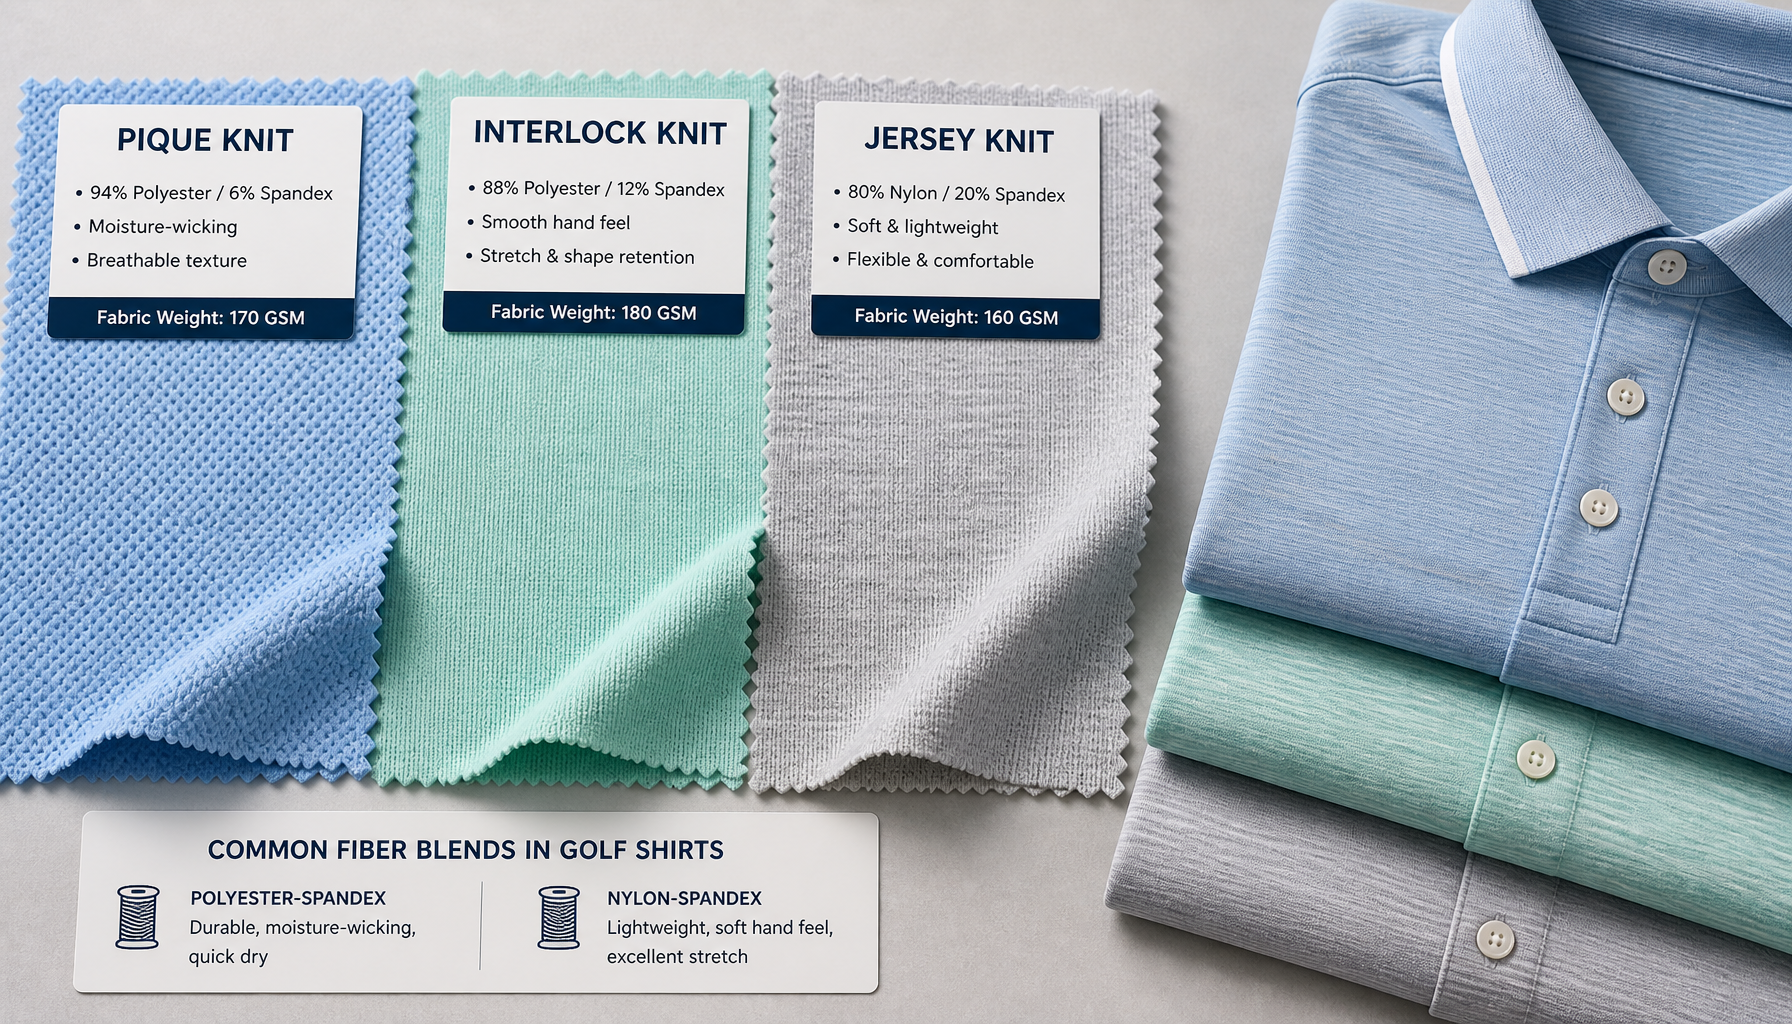
    Pique, interlock and jersey golf-shirt concepts with close-up fabric illustrations
    Structure and styling illustration. Airflow, moisture handling, stretch and durability must be assessed on the selected fabrics; the graphics are not test results.

    Evaluate movement at the shoulder and sleeve

    A golf swing places directional demands on the back, armhole and sleeve. More spandex does not automatically mean easier movement: extension force and pattern geometry both matter. Trial the shirt during address, backswing and follow-through, checking hem lift, placket distortion and pulling across the shoulder.

    For an illustrative strain estimate, a fabric span increasing from 42 cm to 50.4 cm extends by 20%. A laboratory comparison at that extension should examine the force required and subsequent recovery, not merely whether both materials can be pulled to that length. Confirm the actual critical strain on the garment before setting a test condition.

    Separate texture, mass and comfort evidence

    A visibly textured surface does not prove higher air permeability than a smooth one. Compare the candidate fabrics under the same method and preparation. ISO 9237 measures air permeability; drying and liquid-moisture behaviour require different evaluations. If sun protection is part of the sales claim, obtain relevant UV evidence rather than inferring it from colour or density.

    Fabric mass also needs a garment context. If an illustrative shirt contains 0.85 m² of net fabric area, a 160 g/m² material contributes 136 g, while a 190 g/m² material contributes 161.5 g: a 25.5 g difference before trims. This is not purchased marker consumption or total garment weight. Decide whether that difference is meaningful to the brief instead of treating lower GSM as an automatic quality improvement.

    Approve the collar, placket and decoration as an assembly

    The body fabric cannot solve every collar or placket problem. Interfacing, collar construction, sewing feed and component dimensional change affect whether the front stays flat. Wash the assembled sample under the intended care conditions and inspect twisting, puckering, collar shape and differential shrinkage between components.

    Run embroidery or transfer trials at the intended logo size and location. Check local stiffness, distortion, surface damage and durability after care. A logo that looks acceptable on an unstretched swatch may pucker on a lightweight chest panel or restrict movement on a fitted sleeve.

    Choose the production option through a controlled trial

    Shortlist structures using the technical brief, then make comparable garments with documented construction settings. Where pattern or process adjustments are necessary, record them and include their cost. Compare measured usable width, marker consumption, sewing time and the cost of achieving the approved appearance.

    Release the selected fabric against a named construction and finish revision, approved colours, dimensional requirements and garment standard. Keep a retained washed sample for production comparisons. The right structure is the one that meets the shirt’s performance and appearance requirements repeatedly at an acceptable cost, not the one with the most familiar marketing name.

  • How Can Buyers Compare Fabric Quotes When GSM, Width, Composition, and Finishing Are Different?

    How Can Buyers Compare Fabric Quotes When GSM, Width, Composition, and Finishing Are Different?

    Compare fabric quotes only after separating technical suitability from price conversion. A kilogram price, a linear-metre price and a price for a different usable width are not directly comparable. First establish which candidates meet the garment brief. Then convert the quotations to a common basis and calculate the cost of producing acceptable garments.

    Confirm what each price actually buys

    Record currency, price unit, delivery term and named place, tax treatment, quotation validity, minimum order by colour and any surcharges. Confirm whether weight excludes packaging and whether width means full width or usable cutting width. For tubular fabric, establish whether the stated width is laid-flat or opened width before applying any area conversion.

    Ask whether the quoted article includes the approved dyeing and finishing route. A price for unfinished or differently finished material does not cover the same product as a finished fabric ready for cutting. Keep the technical-sheet revision beside the quote so a commercial comparison does not silently compare different constructions.

    Convert kilogram prices using the billed fabric dimensions

    For open-width fabric with consistent mass per area, theoretical kilograms per linear metre = GSM × full width in metres ÷ 1,000. A kilogram quote multiplied by that result gives a theoretical linear-metre price. If invoiced mass includes unusable edges, using only usable width in this conversion understates the cost.

    Usable-area cost is then linear-metre price ÷ usable width in metres. This is a screening calculation, not garment yield. It assumes the quoted weight and width are representative; actual invoiced mass, measured length and agreed usable width should reconcile the production costing.

    Hypothetical quote comparison; these are not supplier offers
    Input or result Fabric A Fabric B
    Quotation $10.00/kg $3.50/linear m
    Finished weight 220 g/m² As specified in B’s approved technical sheet
    Full / usable width 1.65 m / 1.60 m 1.55 m / 1.50 m
    Calculated mass per metre 0.363 kg/m Not needed to convert a metre quote
    Linear-metre price $3.63 $3.50
    Price per usable square metre Approximately $2.27 Approximately $2.33

    B has the lower metre price, while A has the lower usable-area price. Neither result decides the order: both materials still need technical approval, and the cutting marker determines how much each garment consumes.

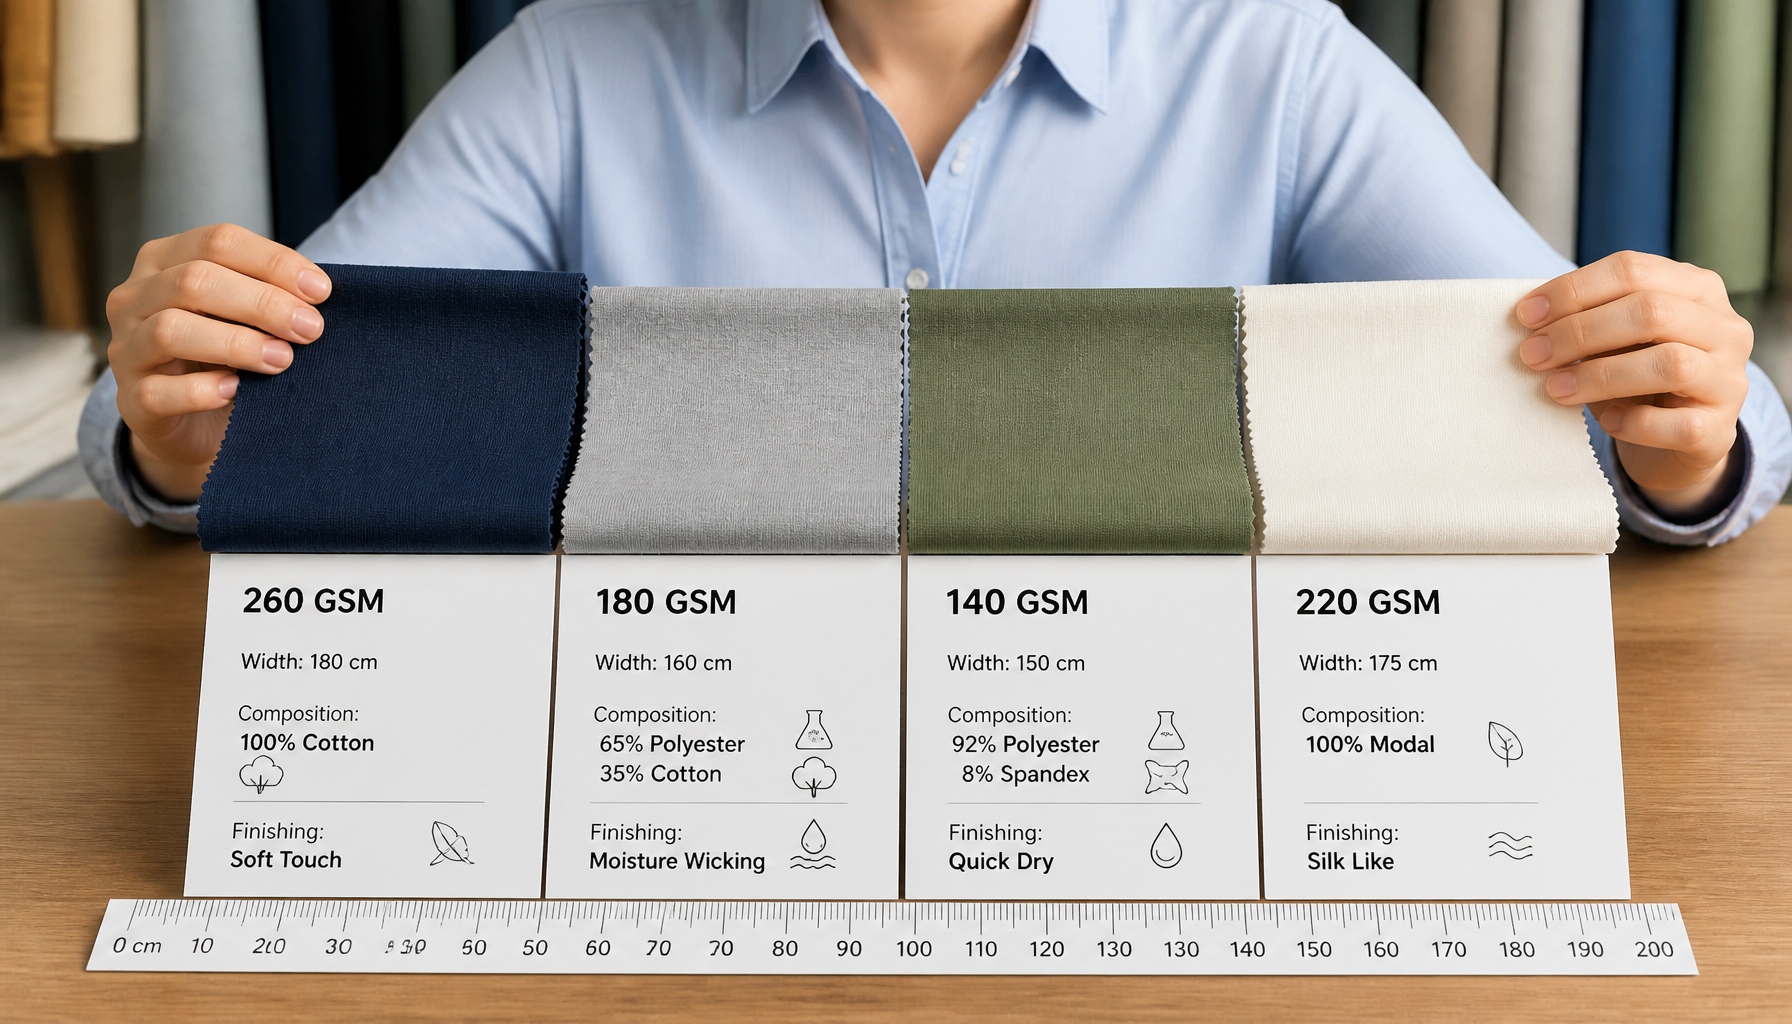
    Fabric swatches displayed with composition, weight, width and finish labels
    Illustrative comparison layout. Printed specifications are not verified quotations or a substitute for the approved technical sheets.

    Run the marker before ranking the fabrics

    Use the actual pattern, size ratio, minimum usable width and any nap or one-way restrictions. A few centimetres of usable width can determine whether another panel fits across the marker. Area cost alone cannot capture that step change.

    Continuing the hypothetical example, suppose approved markers consume 0.90 m per garment for A and 1.00 m for B. Material cost is $3.63 × 0.90 = $3.267 for A and $3.50 × 1.00 = $3.50 for B. A would save about $0.23 per garment under those assumptions. The consumption values must come from actual markers, not from assuming that wider fabric always produces a fixed percentage saving.

    Price the performance gap and process changes

    Different composition, weight and finishing can change support feel, surface durability, decoration compatibility and care behaviour. Remove any candidate that cannot meet a mandatory requirement. If an alternative needs lining, a different seam or an extra finishing operation, cost the revised garment rather than pretending the fabrics are interchangeable.

    Ask whether a claimed moisture-management finish or surface treatment is included in the quote and represented in the sample. Request appropriate evidence for any required durability after care. A soft initial hand feel does not establish equivalent long-term performance.

    Allocate order-level costs without hiding waste

    Sampling, laboratory work, small-lot dyeing charges and freight may be fixed or partly fixed. As an illustration, a $300 order-level charge adds $0.10 per garment to 3,000 accepted garments, but $0.50 to 600. Use the realistic order quantity and distinguish development costs from recurring production costs.

    Define what the consumption figure already includes. If marker consumption includes cutting waste, do not add the same allowance again. Additional roll defects, end losses or rejected garments need separate, justified assumptions. Under an illustrative 98% accepted-garment yield, a production cost of $3.30 per piece started becomes $3.30 ÷ 0.98, or about $3.37 per accepted piece, before any recovery value.

    Make the comparison auditable

    The final comparison should link each price to the approved specification, sample, marker and delivery basis. Show assumptions and unresolved deviations beside the total, not in a separate email chain. Confirm the commercial terms again when quantities, colours or specifications change.

    Select the lowest defensible cost for an acceptable garment, not the lowest isolated price unit. A quote is decision-ready when another buyer can reproduce the conversion and understand exactly which technical and commercial risks remain.

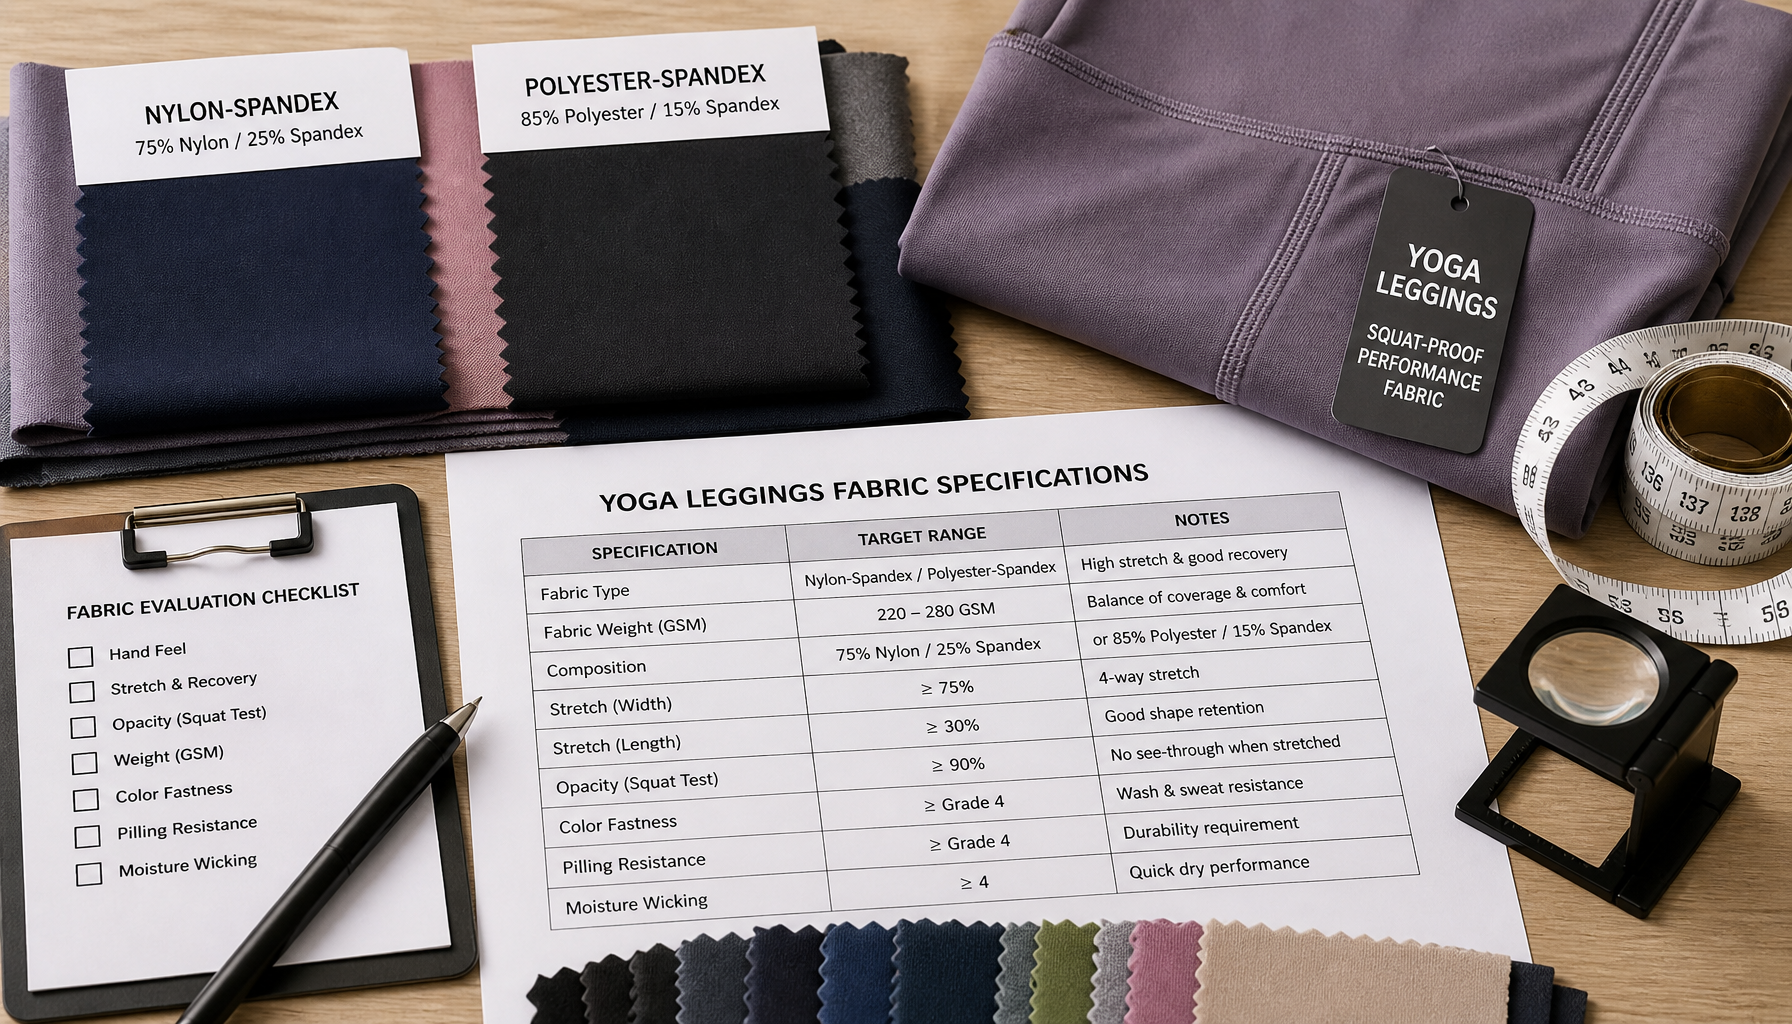
  • How Should Buyers Set Fabric Specifications for Squat-Proof Yoga Leggings Before Requesting Quotes?

    How Should Buyers Set Fabric Specifications for Squat-Proof Yoga Leggings Before Requesting Quotes?

    Specify squat-proof yoga-legging fabric through a defined garment coverage assessment, supported by construction, elasticity and production controls. Do not reduce the brief to a minimum GSM or spandex percentage. Coverage depends on the fabric, colour, pattern strain, seam placement and assessment conditions. A supplier cannot price the requirement reliably if “squat-proof” is the only acceptance instruction.

    Translate the fit into a fabric-strain requirement

    Start with the approved size chart, pattern and intended compression level. Identify high-strain locations during a squat, including the seat, upper thigh and seam intersections. A flat swatch stretched by hand does not reproduce the distribution of strain in a garment.

    In an illustrative example, an 80 cm relaxed garment circumference fitted around a 100 cm body has 20% negative ease relative to the body. The fabric extension is (100 − 80) ÷ 80 × 100 = 25%. Confusing those two percentages can lead to an opacity assessment at insufficient extension. Use pattern calculations to plan the trial, then confirm the critical locations on the finished garment.

    Size grading also matters. Do not assume that approving a medium size establishes coverage in every size. Review where the graded pattern produces the greatest local strain and include those fit conditions in the approval plan.

    Make the coverage assessment reproducible

    Agree the lighting arrangement, viewing distance, backing or underwear contrast, fabric extension, garment movements and pass/fail reference before comparing candidates. Photograph the setup and retain an approved garment for comparison. If appearance is judged visually, record that fact instead of presenting an invented numerical “opacity grade” as a recognised laboratory standard.

    Evaluate relevant colours separately. A dark sample may conceal contrast that is visible through a pale colourway. Include dry and damp conditions when both are relevant to the use claim, and specify the care sequence before reassessment. The objective is a repeatable brand acceptance protocol, not a promise of invisibility under every possible light and viewing angle.

    Connect the specification to the failure risk

    RFQ fields that turn a coverage brief into a testable purchase requirement
    Field What to define Why it matters
    Construction and finish Approved article or construction revision; permitted changes. A finish change can alter hand feel, dimensions and stretched appearance.
    Finished mass and width Agreed GSM range and minimum usable width after the specified preparation. Controls consistency and marker feasibility without treating weight as proof of opacity.
    Elasticity Directions, load or extension, cycles, recovery interval and acceptance limits. Separates support feel from residual growth.
    Coverage Colours, garment sizes, strain locations, lighting and visual reference. Connects the material to the actual product claim.
    Care and durability Wash/dry procedure, evaluation stages and appearance limits. Prevents approval from covering only an unwashed prototype.

    Set numerical limits with the garment team and laboratory using the approved reference and end use. A universal GSM threshold or arbitrary recovery percentage would create false precision rather than a defensible specification.

    Measure support and recovery as different properties

    A high-spandex fabric can feel easy to stretch or relatively firm depending on construction. Request force at a defined extension when support feel matters, and residual extension after a defined recovery period when bagging is the concern. Specify both fabric directions and the relevant care history.

    ISO 20932-1 provides strip-test methods for elasticity. Agree the applicable procedure and conditions with the laboratory; the method name alone does not set a garment pass limit. Pair the report with a wear-and-movement assessment because seams, waistband construction and panel orientation change the finished result.

    Ask for a quote against an approval sequence

    Send suppliers the specification, colour quantities, usable-width requirement, target delivery basis and intended decoration. Ask them to identify deviations explicitly. An alternative composition may be worth testing, but it should not silently replace the quoted reference while retaining its approval status.

    Separate initial sampling, colour approval, pilot-garment approval and bulk release. Require traceable sample identification and confirmation of whether the sample uses the proposed bulk construction and finish. A fabric chosen from stock for a fast fitting is not automatically representative of the later production lot.

    Compare the cost of compliant garments

    Consider an illustrative material option saving $0.20 per metre at 0.90 m consumption: the nominal saving is $0.18 per legging. If that option requires a lining costing $0.45 per garment to meet the coverage brief, it is already $0.27 more expensive before additional sewing. The comparison has changed from two equivalent fabrics to two different garment constructions.

    Release the selected option only when the approved garment, colour scope, test records and bulk specification agree. Hold approval when the supplier can offer only a GSM number, a stretched-hand photograph or a generic “squat-proof” statement. The purchase requirement is demonstrable coverage in the intended leggings, with controlled repeatability across the order.

  • What Happens Between Fabric Sampling and Bulk-Production Approval?

    What Happens Between Fabric Sampling and Bulk-Production Approval?

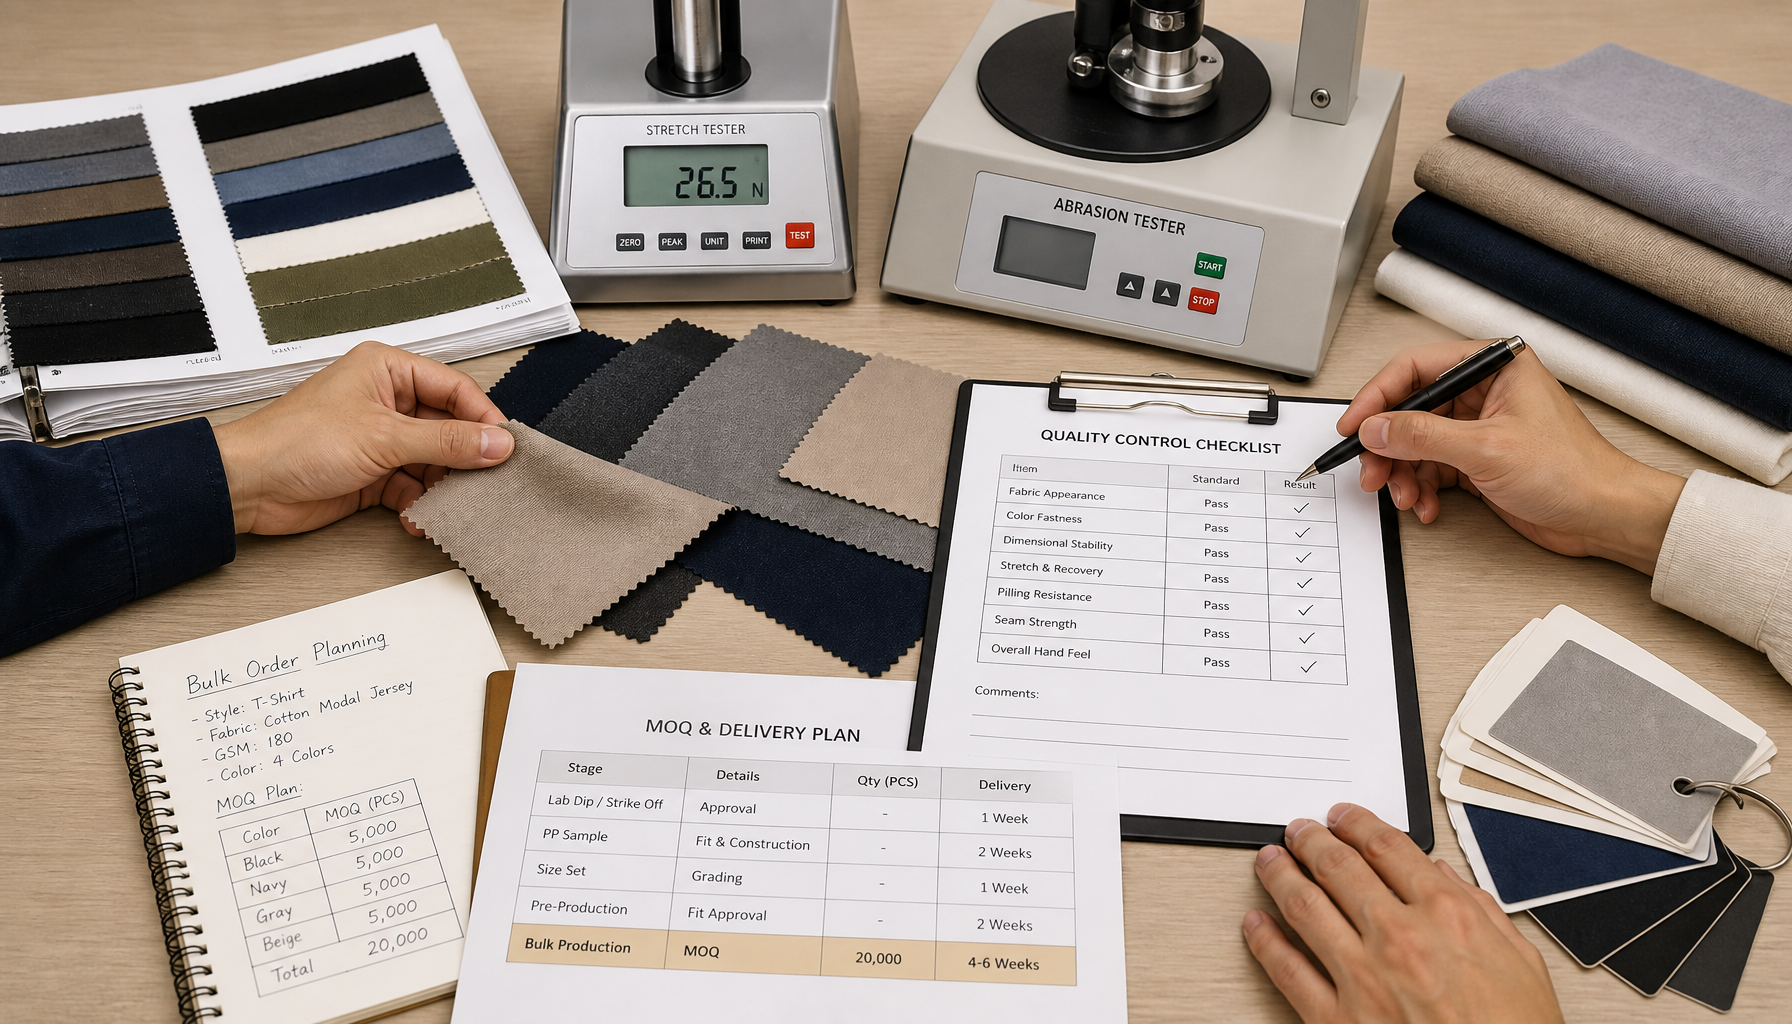
    The approval phase between fabric sampling and bulk production is where technical claims become a measurement file. A sample shows that a construction is possible; an approval record states what will be delivered in bulk, how it will be measured, and which deviations will be rejected. In knitted spandex programs — nylon or polyester spandex for lingerie, sportswear, yoga wear and shapewear — this file decides both the landed cost per garment and the risk the buyer carries until the last roll is cut.

    The phase ends with four signed documents rather than one stamp: a sealed sample in the buyer’s colour, a specification sheet covering GSM, nominal width and usable width with tolerances, a colour approval signed under a defined light source, and a test-and-sampling plan that names the methods and the accept or reject limits. Every bulk roll is judged against those four, so all of them should be in place before the first bulk lot enters the dyeing machine.

    Four approval gates and what each one releases

    Sampling and bulk approval are not one decision. They are four gates, each releasing a different risk. Treating them as a single “approved” status is the usual reason a repeat order arrives with a handfeel that no longer matches the sample that won the business.

    Typical gates for a knitted spandex program. Durations are working-day ranges for an existing, repeatable construction and are planning figures rather than commitments.
    Gate Evidence produced Typical duration What it locks
    1. Lab dip and handfeel Dips submitted under the agreed light source; a handfeel reference retained by both parties 3–7 working days per round Colour standard and surface reference
    2. Sample yardage and garment trial Fabric from a pilot lot, cut and sewn by the garment maker; opacity, stretch and recovery measured on the finished piece 7–14 working days Construction judged against the garment, not against a flat swatch
    3. Test plan and tolerance sign-off Named test methods, sampling frequency, AQL and reject limits 3–5 working days The measurement rules used at inspection
    4. Pre-production lot approval First bulk lot sampled and tested against gates 1–3; shade band and roll plan confirmed Runs in parallel with bulk dyeing, typically 15–25 working days Release of the bulk run and the repeat-order baseline
    Fabric sampling and bulk approval workflow with sample lots and production rolls
    Sampling and bulk approval form one loop: sample, measure, approve, then measure the first bulk lot against the same numbers.

    What a sample has to prove before gate 3 can be signed

    Approving on appearance alone leaves the specification undefined. Six properties decide whether a knitted spandex fabric behaves the same way in bulk, and each one needs a method and a number before it can be accepted or rejected.

    Mass per unit area
    Measured with a 100 cm² cutter to ISO 3801. A 120 gsm fabric delivered at 114 gsm is 5% less material per square metre: enough to change opacity on a light colour and to move the cost per garment even when the price per metre does not change.
    Dimensional stability
    Washed and dried to ISO 6330 and measured to ISO 5077. Spandex knits are commonly specified at no more than 3% length and width change, with 5% accepted where the garment is cut loose and the pattern allowance absorbs it.
    Stretch and recovery
    Extension and growth measured to ASTM D2594 for low-power knits, or ASTM D6614 where the program measures elastane-rich high-stretch fabric. Recovery above 90% at the agreed extension is a common requirement for leggings and swimwear, because growth after wear appears as bagging at the knee and seat.
    Colour fastness
    Wash, rubbing and perspiration to ISO 105-C06, ISO 105-X12 and ISO 105-E04. Grade 4 on the grey scale covers most apparel programs; swimwear and deep shades are often written at grade 4–5 because chlorinated and salt water accelerate bleeding.
    Surface behaviour
    Pilling and snagging to ISO 12945-2. Grade 3–4 and above is typical for cut-and-sew sportswear. Brushed surfaces, loop structures and open-filament yarns lower the result, so the test belongs on the finished surface rather than on a flat swatch.
    Usable width, not nominal width
    Nominal width includes the edge that will be trimmed or rejected. A 165 cm fabric with 2 cm edge bands offers roughly 161 cm of usable width, and every yield calculation should be run on that figure.

    Worked example: what one 150 kg lot of a 120 gsm cooling knit covers

    Take a summer base-layer program that needs a light matte knit with a cooling finish. The candidate construction is H213, an 85% nylon / 15% spandex knit at 120 gsm and 165 cm, quoted at a nominal yield of 5.0 m/kg with a 150 kg minimum per colour. The approval question is not whether the swatch feels right; it is whether one minimum lot covers the pilot run, and what the buyer owns if it does not.

    1. Usable width. 165 cm nominal minus 2 cm of edge trim on each side leaves 161 cm usable (assumed trim; confirm against the finished roll).
    2. Mass per linear metre. 0.120 kg/m² × 1.61 m = 0.193 kg/m.
    3. Catalogue yield against the physics. 1 ÷ 0.193 ≈ 5.2 m/kg theoretical. The quoted 5.0 m/kg already carries the finishing and sampling allowance, so planning above 5.0 m/kg plans into a shortage.
    4. What 150 kg buys. 150 kg × 5.0 m/kg = 750 m of usable fabric.
    5. Garment coverage. At 0.60 m per garment plus 8% spare (0.648 m), 750 m covers about 1,150 pieces — a pilot run, not a season (assumed consumption and spare rate; replace with the marker consumption from the buyer’s CAD file).

    Two decisions follow from that arithmetic. Colours must be approved before the lot is dyed, because re-dyeing 150 kg for a colour change consumes a full dyeing cycle and risks a shade break against the approved dip. And if the program grows past roughly 1,150 pieces, the next lot is a new dyeing lot with its own shade band, which belongs in the approval record rather than in a surprise at final inspection.

    Where programs lose money between sample and approval

    • Approving colour under undefined lighting. A dip that matches in an office can read red under D65 and green under TL84. Name the light source on the approval, submit the dip under both, and record the measured difference: ΔE ≤ 1.0 against the standard is a common laboratory-dip target, with bulk lots accepted in a wider band such as ΔE ≤ 2.0.
    • Approving a hand sample the production line cannot repeat. Hand-knitted and pilot-machine swatches hide the tension and heat-setting behaviour of a production line. Require gate 2 yardage to come from the same knitting machines, dyeing machine and finishing line that will run the order.
    • Locking colour but not width or GSM. A lot that arrives 5% light in GSM and 2 cm narrow removes material from every garment while the price per metre stays fixed. Both tolerances belong on the same sheet as the colour reference.
    • Testing only the first lot. Dye lots drift after two or three cycles. Keep a retained sample per lot and re-test every third or fifth lot on the properties that reach the garment: shade, GSM, width and stretch recovery.
    • Leaving both test layers to the garment factory. Fabric-level results (GSM, width, dimensional change, stretch) and garment-level results (appearance after wash, seam slippage, opacity on the finished piece) fail for different reasons. Split the responsibility in writing, or a claim is resolved by the mill and the garment maker blaming each other.

    Why MOQ is a machine number, not a sales threshold

    Minimum order quantities for dyed knit fabric come from the dyeing vessel, not from a negotiating position. A 500 kg overflow machine running at one third of a batch is roughly 150–200 kg, which is why 150 kg per colour is a common floor for a single shade. The consequence for the buyer is arithmetic:

    • Six colours at 150 kg each is 900 kg before the first garment is cut.
    • The same 900 kg in three colours is 300 kg per colour, with fewer dye lots and a lower probability of a shade break between lots.
    • Fewer colours with more metres per colour lower the cost per metre, because machine time, laboratory work and lot administration spread over more fabric.

    The practical move is to align the colour count with the first production plan before the sampling stage closes. Keeping a colour that will sell 200 garments is not a quality decision; it is a decision to fund extra dye lots.

    Acceptance standards to write into the approval

    Common acceptance items for knitted spandex. These bands are usual industry starting points and should be replaced by the program’s own numbers wherever a customer standard exists.
    Item Method Typical acceptance
    Usable width Measured on each roll, three points minimum Nominal ± 2 cm, with usable width stated separately
    Mass per unit area ISO 3801, 100 cm² cutter Nominal ± 5%
    Dimensional change ISO 6330 + ISO 5077 ≤ ± 5%, commonly ≤ ± 3% for spandex knits
    Stretch and recovery ASTM D2594 or ASTM D6614 Recovery ≥ 90% at the agreed extension
    Colour fastness ISO 105-C06, ISO 105-X12, ISO 105-E04 ≥ grade 4 on the grey scale
    Pilling and snagging ISO 12945-2 ≥ grade 3–4
    Surface defects Four-point system, assessed per roll ≤ 20 points per 100 yd², threshold agreed in the record
    Fabric swatch, specification sheet and test report prepared for bulk production approval
    An approval package that can be re-measured: sealed sample, specification with tolerances, and the test report from the same lot.

    What the approval record should contain

    • Fabric code, composition, and the reference number of the sealed sample held by both parties
    • GSM with tolerance, nominal width, usable width, and yield expressed in m/kg
    • Colour reference, the light source used for approval, and the measured difference from the standard
    • Test methods, sampling frequency and accept or reject limits for every property in the table above
    • Defect classification, and the rework, replacement or credit path for a lot that fails
    • Spare allowance, roll length, put-up and packing specification
    • Sampling and production lead times, and the dyeing capacity reserved for repeat lots
    • Payment milestones tied to bulk approval rather than to shipment, with the repeat-order baseline attached

    Questions buyers ask before signing

    Does approval freeze the fabric for the life of the program?

    No. It freezes the specification and the reference sample for the lots named in that approval. A change of yarn supplier, finishing route or dyeing machine creates a new approval, and programs that state this in the record can measure the next lot against the same numbers instead of arguing about what the sample looked like.

    How long does the whole stage take?

    Three to six weeks for an existing construction: one or two lab-dip rounds at 3–7 working days each, 7–14 working days for sample yardage and the garment trial, then 3–5 working days to sign the test plan. Bulk dyeing runs in parallel with gate 4, typically 15–25 working days after colour and finish confirmation.

    Who pays for a second round of dips?

    The first round is usually included in the quotation and later rounds are charged per dip. Put the number of included rounds in the quotation, because the charge matters most in the case where a colour changes after the bulk lot has been dyed.

    Key takeaways

    • Treat sampling, testing, MOQ and quality alignment as four separate releases, each with its own evidence.
    • Approve on numbers — GSM tolerance, usable width, dimensional change, stretch recovery, colour fastness — each with a stated method.
    • Run yield calculations on usable width and on the quoted m/kg, never on the theoretical figure.
    • Size the colour count against the first production plan so the MOQ arithmetic works before the design is locked.
    • Write the repeat-order baseline into the approval record, including the light source and the retained samples.
  • How Can Buyers Verify the Strike-Off Approval Process Before Paying a Fabric Deposit?

    How Can Buyers Verify the Strike-Off Approval Process Before Paying a Fabric Deposit?


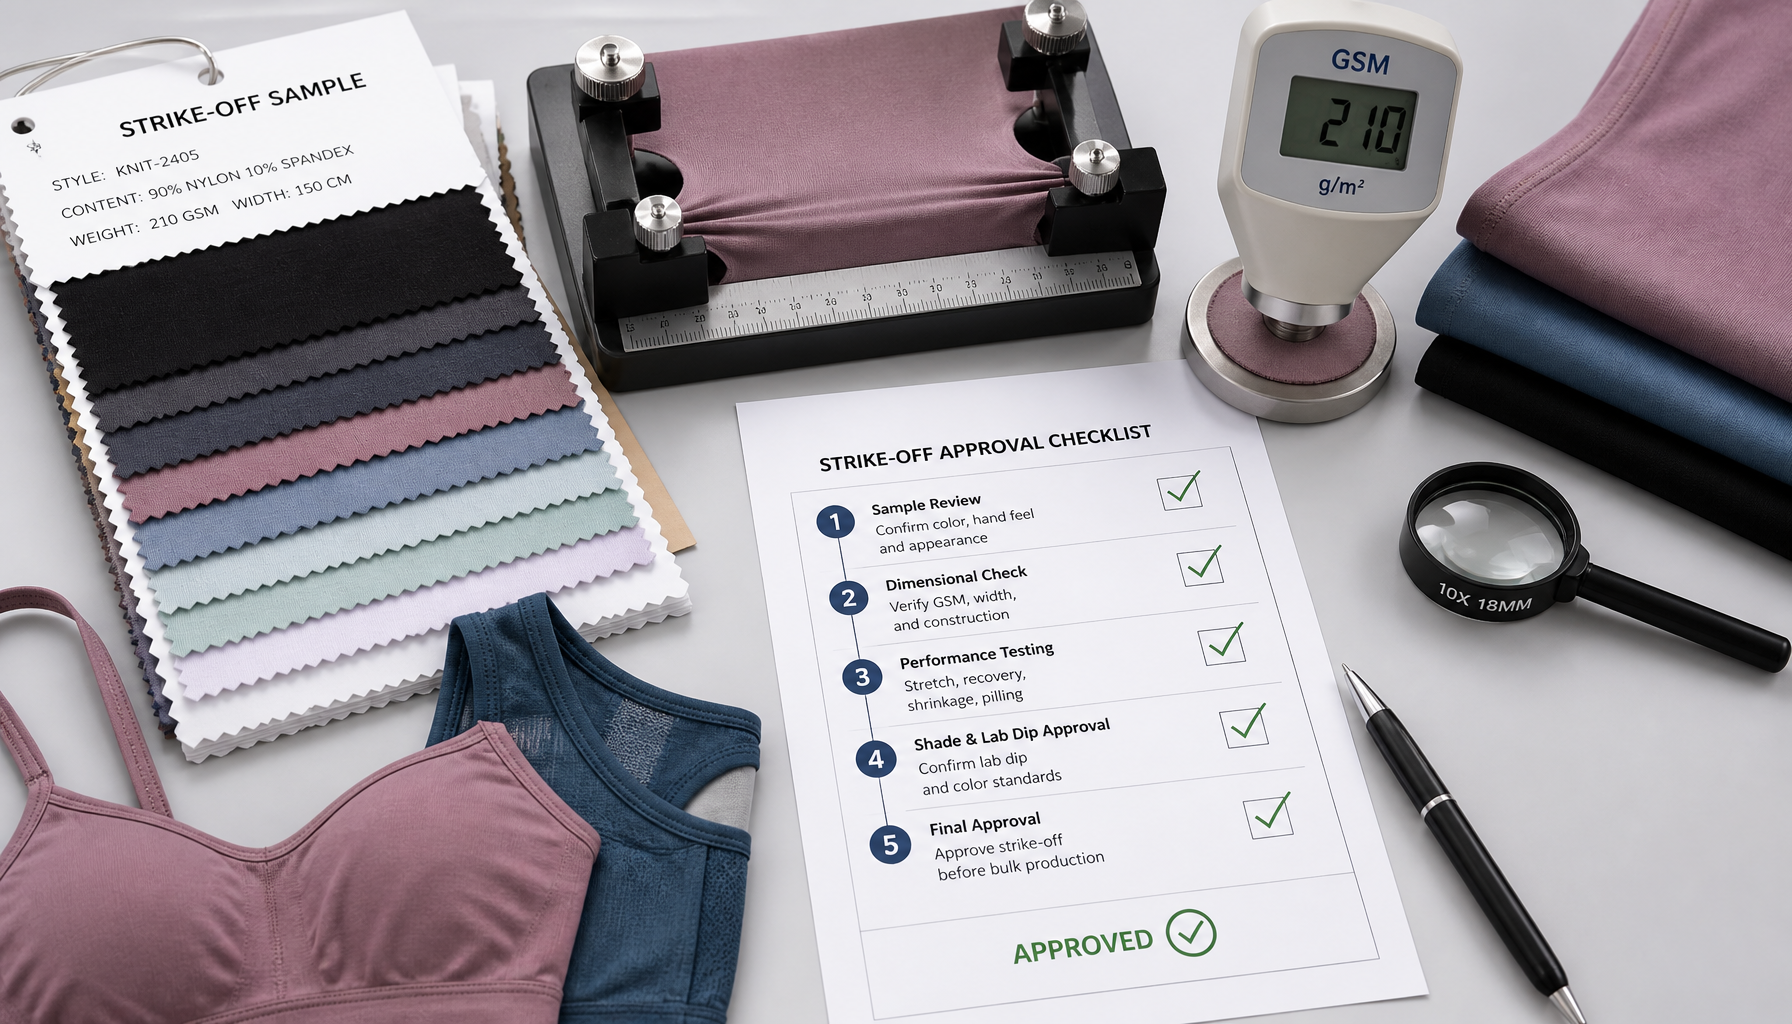
    Before paying a fabric deposit, buyers should obtain a written approval matrix that defines the sample type, reference standard, acceptance criteria, revision responsibility, approval authority, and the exact event that authorizes bulk production. For printed fabric, that sample may be a strike-off; for a solid dyed nylon-spandex or polyester-spandex fabric, the relevant color approval is usually a lab dip rather than a strike-off.

    Fabric sample presented for strike-off approval

    Confirm what the supplier means by “strike-off”

    Terminology must be resolved before discussing payment. A strike-off normally shows how a print artwork, color combination, scale, and placement reproduce on a specified fabric. It is not automatically a first article, a bulk-lot sample, or proof that the finished fabric meets every performance requirement.

    Use the correct approval item for the decision being made:

    Buyer requirement Appropriate approval item What it confirms
    Solid dyed color Lab dip or another agreed color submission Shade direction under the agreed viewing conditions
    Printed artwork Strike-off Print color, repeat, scale, registration, and visual reproduction on the submitted base fabric
    Hand feel or finish Finished development swatch or sample yardage Surface, drape, hand, and the proposed finish
    Fabric construction Identified development sample with a specification sheet Composition, knit structure, GSM, width, and stretch response of that sample
    Bulk conformity Pre-production or bulk-lot approval defined in the purchase agreement Whether production material matches the approved references and tolerances

    A buyer may need more than one approval item. Approving a print strike-off does not automatically approve GSM, usable width, stretch recovery, dimensional stability, colorfastness, or bulk shade consistency.

    Color and print strike-off samples under review

    Build a traceable approval package

    The supplier should identify every submission with information that links it to the order. At minimum, the approval package should record:

    • buyer style or project reference;
    • supplier fabric code and base-fabric specification;
    • artwork file name, version, repeat size, and orientation for printed designs;
    • color reference and viewing conditions;
    • submission number and date;
    • proposed finish and any optional treatment;
    • physical sample location or courier reference;
    • approver's name, decision, date, and written comments.

    Use one status for each submission: approved, approved with stated conditions, or rejected with correction instructions. Avoid comments such as “close,” “almost right,” or “proceed carefully,” because they do not define whether the supplier is authorized to continue.

    Define acceptance criteria before the sample is produced

    The approval criteria should match the type of submission. For a printed strike-off, buyers may need to confirm:

    • print colors against the named reference under an agreed light source;
    • artwork scale, repeat, direction, and placement;
    • registration between colors and sharpness of printed details;
    • strike-through, surface coverage, and appearance when the fabric is extended;
    • hand-feel change caused by ink, binder, curing, or another print process;
    • whether the submitted base fabric matches the intended construction.

    If instrumental color measurement is required, identify the instrument conditions, specimen preparation, color-difference formula, and tolerance in the agreement. There is no responsible universal ΔE limit for every fabric, shade, customer, and end use.

    For stretch activewear, inspect the print both relaxed and at the extension expected in the garment zone. A print that appears continuous on a table may show white grinning, cracking, distortion, or loss of detail when used across a seat, thigh, waistband, or sports-bra panel.

    Separate visual approval from fabric-performance approval

    A strike-off is usually too small to establish every bulk-performance result. Keep a separate checklist for the finished fabric specification, including the requirements relevant to the product:

    • composition, knit construction, finished GSM, and usable width;
    • stretch and recovery by direction under defined conditions;
    • dimensional stability and spirality after the agreed care cycle;
    • colorfastness, pilling, abrasion, or snagging requirements;
    • moisture-management or other functional claims, where applicable;
    • bulk shade, print, and lot-consistency controls.

    The contract should state which results are needed before bulk production, which can be checked on the first production lot, and what happens if the result falls outside the agreed tolerance.

    Link the deposit to written commercial terms

    Do not assume that a deposit is automatically refundable when a strike-off is rejected. Some suppliers require payment before development work begins; others charge a separate sampling fee or credit approved development costs against the order. The correct arrangement is the one recorded in the quotation, pro forma invoice, purchase order, or development agreement.

    Before payment, confirm in writing:

    1. what the deposit pays for;
    2. whether strike-off or lab-dip costs are included;
    3. how many submissions or correction rounds are included;
    4. who pays for additional revisions, courier charges, screens, cylinders, artwork preparation, or other setup costs;
    5. whether any amount is refundable, non-refundable, or credited to bulk production;
    6. what happens if the buyer rejects the submission or changes the brief;
    7. whether material purchasing or production capacity is reserved before final approval;
    8. which written approval authorizes bulk production.

    Illustrative approval-loop calculation

    Assume a hypothetical program has three print colorways and the agreement includes an initial strike-off plus one correction for each colorway. The planned submission capacity is:

    3 colorways × 2 submissions = 6 strike-off submissions

    This is a planning example, not a ClothFactory commercial term. It shows why the number of colorways and included revision rounds should be written into the quotation before the deposit is paid.

    Use a no-production-without-approval control

    The safest workflow separates sample approval from bulk authorization:

    1. Buyer issues the confirmed artwork, color references, base-fabric specification, and acceptance criteria.
    2. Supplier acknowledges the submission scope, charges, timing, and revision terms.
    3. Supplier produces an identified strike-off, lab dip, or development sample.
    4. Buyer records an approval decision against that exact submission.
    5. Supplier confirms any conditions and the final approved reference.
    6. Buyer issues written authorization for bulk production according to the payment agreement.
    7. Supplier retains the approved reference for bulk comparison and quality control.

    An email or approval form should state that silence, courier receipt, or payment alone does not constitute visual approval unless the commercial agreement explicitly says otherwise.

    Red flags before paying a deposit

    • The supplier cannot explain whether the approval item is a strike-off, lab dip, sample yardage, or bulk-lot sample.
    • The quotation does not identify the base fabric, colorways, revision rounds, or setup charges.
    • The supplier asks for “approval” without a submission code or physical reference.
    • Print scale, repeat, stretch condition, and viewing light are left undefined.
    • The deposit terms do not state whether development charges are refundable or creditable.
    • Bulk production can begin without named written authorization.
    • The supplier treats strike-off approval as proof of all fabric-performance requirements.

    Procurement next step

    Before paying, send the supplier a one-page approval matrix covering the sample type, base-fabric code, artwork version, color references, acceptance criteria, revision rounds, charges, decision authority, and bulk-release point. For a ClothFactory development request, also identify whether the project uses an existing nylon-spandex or polyester-spandex base fabric or requires a new construction; the strike-off should be evaluated on the same confirmed base fabric intended for production.

  • When Should Brands Retest Drying Rate for Repeat Fabric Orders?

    When Should Brands Retest Drying Rate for Repeat Fabric Orders?


    Brands should retest drying rate when a repeat order changes the fiber, yarn, knit construction, GSM, finish, color process, production route, care condition, or performance claim—or when incoming inspection indicates that the new lot no longer matches the approved reference. If the specification and controlled process remain unchanged, the retest frequency should follow a written risk-based quality plan rather than an unsupported assumption that every repeat order is identical.

    Finished activewear fabric prepared for drying-rate verification

    Establish a baseline before setting the retest rule

    The first approved production should create a traceable reference. Record the fabric code, composition, knit construction, finished GSM and width, color, finish, care cycle, conditioning, test method, specimen preparation, water application, endpoint, and result. Retesting cannot confirm consistency if the original approval conditions are missing.

    Keep drying rate separate from wicking, absorbency, and multidirectional moisture transport. These properties may interact, but one result does not substitute for another. If the product claim is “quick dry,” the purchase specification should identify the exact method and acceptance criterion used to support that claim.

    Retest after a material or construction change

    Retest when the repeat order changes any variable that can alter water uptake, spreading, evaporation area, or fabric mass. Relevant changes include:

    • fiber composition or supplier-declared raw material;
    • yarn count, filament structure, texturing, or yarn source;
    • knit construction, density, thickness, finished GSM, or width;
    • spandex content or fabric stretch that changes the exposed surface under wear;
    • brushing, sanding, calendaring, heat setting, or other surface treatment;
    • moisture-management, softening, anti-odor, or other chemical finish;
    • garment care instruction when testing includes laundering.

    A matching composition label is not evidence that two constructions dry at the same rate. Polyester-spandex and nylon-spandex fabrics can each behave differently when yarn, loop geometry, GSM, or finishing changes.

    Retest after a production-process change

    The supplier should notify the buyer when production moves to a different mill, machine group, dyeing route, finishing line, or subcontracted process. Retesting is also appropriate after a major recipe adjustment, equipment change, prolonged production interruption, or corrective action related to moisture performance.

    The purpose is not to distrust every process change. It is to verify that the approved product claim still applies after a variable with technical relevance has changed.

    Repeat fabric lot being checked against an approved drying-rate reference

    Use a risk-based rule for new colors and dye lots

    A new dye lot does not automatically prove that drying performance changed, but color depth, auxiliaries, finishing conditions, and heat history may affect the finished result. The retest rule should reflect how the performance is achieved.

    Repeat-order condition Recommended action Reason
    Same construction, finish, color route, and controlled production Verify according to the agreed periodic or lot-based quality plan Confirms continued control without treating every reorder as a new development.
    New color family or materially different shade depth Retest a representative finished lot Dyeing and finishing conditions may differ from the approved reference.
    Finish is responsible for the drying claim Retest after finish application and after the agreed wash condition Confirms initial performance and finish durability.
    Mixed dye lots or production groups in one order Keep samples traceable and test representative groups Prevents an average from hiding one nonconforming group.
    Incoming GSM, width, hand, or appearance has shifted Hold approval and investigate before relying on the previous result The shift may indicate a construction or process change.
    Complaint, failed garment test, or abnormal production result Retest retained and current samples under the same method Helps separate fabric variation from garment, laundering, or test variation.

    For claim-critical garments, the purchase agreement may require verification on every lot. For lower-risk products with demonstrated process stability, periodic testing may be appropriate. The buyer and supplier should agree the frequency before production rather than deciding after a disputed result.

    Keep retest conditions identical to the baseline

    Drying-rate results are sensitive to specimen preparation and environment. Record and control:

    • specimen size, orientation, and number;
    • conditioning temperature and humidity;
    • starting dry mass where the method uses mass;
    • amount and application method of test liquid;
    • support surface, airflow, temperature, and relative humidity during drying;
    • timing interval and endpoint definition;
    • whether the fabric is relaxed, extended, new, or laundered;
    • method edition, equipment, and any deviation.

    Changing the endpoint from “time to a defined residual moisture level” to “mass lost after a fixed time” creates a different measurement. The repeat-order result must use the same definition as the approved baseline.

    Illustrative calculation for a mass-loss method

    The following is an illustrative calculation, not a ClothFactory test result or a universal test method. Suppose a controlled procedure records a specimen at 12.0 g immediately after wetting and 9.6 g after 20 minutes:

    Water mass lost = 12.0 g − 9.6 g = 2.4 g

    Average mass-loss rate = 2.4 g ÷ 20 min = 0.12 g/min

    This value is comparable only with specimens tested using the same fabric area, water dose, conditioning, airflow, timing, and endpoint. It does not by itself prove that the garment will feel dry during wear.

    Investigate the result before rejecting the lot

    If the repeat lot differs from the baseline, first confirm that the laboratory conditions, specimen preparation, and calculation are consistent. Then review lot traceability, GSM, construction, finish add-on where applicable, color route, heat-setting history, and wash condition.

    Retest matched retained and current specimens when possible. A retained reference tested in the same session helps show whether the difference comes from the fabric or the test environment. Do not discard the original result or repeatedly retest until one specimen passes; retain every result and document the disposition.

    Information buyers should include in the repeat-order specification

    Provide the supplier or laboratory with:

    • approved fabric code and sealed reference;
    • composition, knit construction, finished GSM, width, color, and finish;
    • intended garment and moisture-related claim;
    • drying-rate method, edition, specimen count, and conditioning;
    • water dose, timing, endpoint, and acceptance tolerance;
    • required prewash or number of wash cycles;
    • lot definition and roll-selection rule;
    • change-notification requirements;
    • retest frequency and action after a failed or borderline result.

    Procurement next step

    Create a change-control list for every repeat fabric order and compare it with the approved baseline before releasing production. Retest immediately when a relevant material, construction, finish, process, shade route, care condition, or claim changes; otherwise follow the agreed periodic or lot-based verification plan. ClothFactory can provide identified nylon-spandex or polyester-spandex samples for comparison, but the buyer and supplier should agree the method, baseline, frequency, and acceptance rule before treating drying performance as consistent.

  • How Many Samples Should Buyers Test When Checking Stretch Ratio?

    How Many Samples Should Buyers Test When Checking Stretch Ratio?


    There is no universal sample count for checking fabric stretch ratio. Buyers should define the count by testing stage, lot structure, fabric direction, and the selected method; one swatch can screen a construction, but it cannot demonstrate consistency across a production lot.

    Stretch fabric specimens prepared for ratio and recovery testing

    Count rolls, sampling locations, and specimens separately

    A useful sampling plan distinguishes three units:

    • Rolls sampled: shows whether results vary across the lot.
    • Locations within a roll: detects beginning-to-middle-to-end variation or local finishing differences.
    • Test specimens: provides repeat measurements under the same method.

    Reporting only “nine samples tested” is incomplete. Nine specimens cut beside each other from one roll provide repetition, but they do not represent three rolls or multiple dye lots.

    Use the testing stage to set the sampling plan

    Testing stage Decision being made Sampling approach
    Initial fabric screening Is this construction worth developing? Take specimens in both principal directions from more than one location on the available sample length. Treat the result as preliminary.
    Development or lab-dip approval Does the finished fabric still match the target after dyeing and finishing? Compare specimens from the approved development lot under the same conditioning, extension, hold, and recovery conditions.
    Pre-production confirmation Is the planned construction repeatable before bulk cutting? Sample across available rolls or production positions rather than increasing repetitions from one small area.
    Bulk-lot acceptance Does the shipment meet the agreed specification? Use a written roll-selection plan based on lot size, dye lots, machine positions, and order risk. Follow the specimen count required by the chosen test method.

    The exact count should be written into the purchase specification or quality agreement. If the governing test method specifies a minimum number of specimens, that requirement takes priority over an informal buyer checklist.

    A practical screening example

    The following is an illustrative buyer-defined plan, not an industry standard or ClothFactory test result:

    1. Select three locations across the available sample length.
    2. Cut three specimens in the main direction and three in the crosswise direction from each location.
    3. Test all specimens under identical conditioning, gauge length, extension, hold time, and recovery time.
    4. Report each result, the average, and the range; do not report only the best value.

    This plan produces 18 measurements:

    3 locations × 3 specimens × 2 directions = 18 measurements

    It can reveal local and directional variation during development. It does not prove bulk-lot consistency because all specimens may still come from one roll. For bulk approval, spread the sampling across the rolls and production groups that make up the shipment.

    Stretch knit specimen being measured under controlled extension

    Define stretch ratio before comparing results

    Stretch ratio should be calculated from a stated original gauge length and a stated extension condition. A common calculation format is:

    Stretch (%) = (extended length − original length) ÷ original length × 100

    Illustrative calculation: if a marked section increases from 100 mm to 150 mm under the defined load or extension procedure:

    (150 mm − 100 mm) ÷ 100 mm × 100 = 50% stretch

    The number is meaningful only when the direction, specimen dimensions, load or extension procedure, extension rate, hold time, conditioning, and equipment are recorded. Results produced with different conditions should not be treated as equivalent.

    Measure recovery as a separate result

    High stretch does not guarantee that a fabric returns to its original dimensions. Record the specimen length after the specified recovery period and calculate residual growth separately:

    Growth (%) = (recovered length − original length) ÷ original length × 100

    For example, if the original gauge length is 100 mm and the specimen measures 104 mm after the agreed recovery period, the illustrative residual growth is 4%. This does not establish a universal pass limit. The acceptable result depends on the garment's fit, support requirement, pattern reduction, and use zone.

    Keep every comparison condition consistent

    Stretch results can change when any of these variables change:

    • main versus crosswise direction;
    • specimen width and gauge length;
    • applied load or target extension;
    • extension rate and number of cycles;
    • hold time and recovery time;
    • temperature, humidity, and conditioning period;
    • testing before or after the specified wash cycle;
    • fabric location, dye lot, finish, and roll history.

    The laboratory report should identify these conditions. A hand-pull comparison can help reject obviously unsuitable samples, but it is not a reproducible acceptance test.

    Investigate variation instead of hiding it in an average

    An average can mask one weak roll or one unstable direction. Review the individual values and the range between the highest and lowest results. If one group differs materially, check whether it corresponds to a roll, dye lot, machine position, sample location, or test setup.

    Do not combine results from different fabric constructions, finishes, colors, or wash histories into one average. Dark shades, surface treatments, and heat-setting conditions may affect the finished response, so each approved production group should remain traceable.

    Information buyers should include in the request

    Provide the supplier or laboratory with:

    • fabric code, composition, knit construction, finished GSM, and usable width;
    • intended garment and the body zone where stretch matters;
    • main and crosswise stretch targets;
    • recovery or growth requirement and measurement time;
    • selected test method and any buyer-specific conditions;
    • wash or conditioning procedure;
    • lot definition, number of rolls, and roll-selection rule;
    • required report format, including individual results, average, and range.

    For leggings, sports bras, lingerie, and shapewear, also state the expected garment extension and support level. The same stretch percentage can be acceptable for one product and unsuitable for another because pattern reduction, seam placement, and pressure requirements differ.

    Procurement next step

    Start with a documented development plan that covers both fabric directions and more than one sample location. Before bulk approval, expand the plan across representative rolls and production groups, then test under one agreed method. ClothFactory can prepare identified nylon-spandex or polyester-spandex samples for comparison, but the buyer and supplier should agree the specimen count, lot coverage, test conditions, and acceptance limits before relying on the results.